
Great packaging is the silent salesman along the retail aisle. But before it sits on a shelf, it has to be manufactured. That distinct shape, the satisfying snap of a lid, the precise window revealing the product—none of that happens without die cutting.
For many brands, this stage is a black box. You send a digital file to a factory, and you hope for the best. But ignoring the mechanics—the difference between flatbed and rotary, or how creasing works against the grain—often leads to ballooning costs and “defective” boxes that simply won’t fold straight.
This guide pulls back the curtain on the manufacturing floor. We aren’t just defining terms here; we are breaking down the ROI of different cutting methods. Whether you are troubleshooting a production bottleneck or looking to scale your first run of custom labels, understanding how the blade meets the board is your competitive edge.
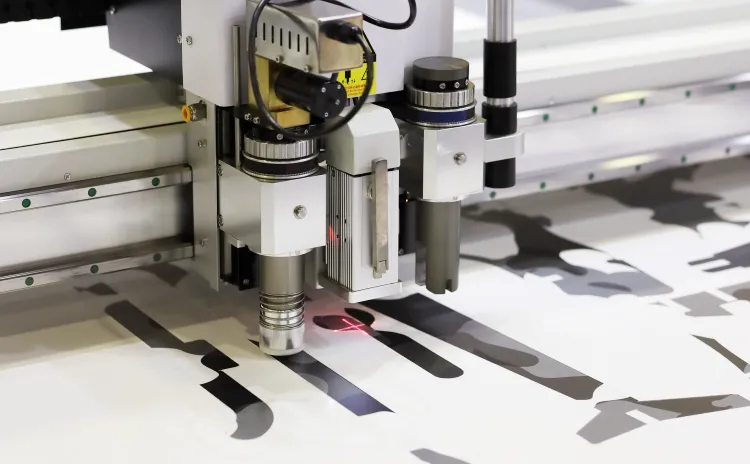
What is Die Cutting in Packaging?
Die cutting transforms flat materials into precise packaging shapes you see everywhere—from folding cartons to product labels. The process relies on a die, which is a hardwood board embedded with sharpened steel rules. Think of it as an industrial-scale cookie cutter, but built for manufacturing precision.
Here’s how the basic components work together:
-
Steel Rules: These blades are hammered into the die board in specific patterns. Through-cutting rules slice all the way through the material. Creasing rules create parallel stress lines that enable clean folding. Perforating rules punch controlled hole patterns for easy tear-away sections.
-
Ejectors: Rubber or foam pieces glued around the die board push the cut material away after each press. This prevents jams and keeps production flowing.
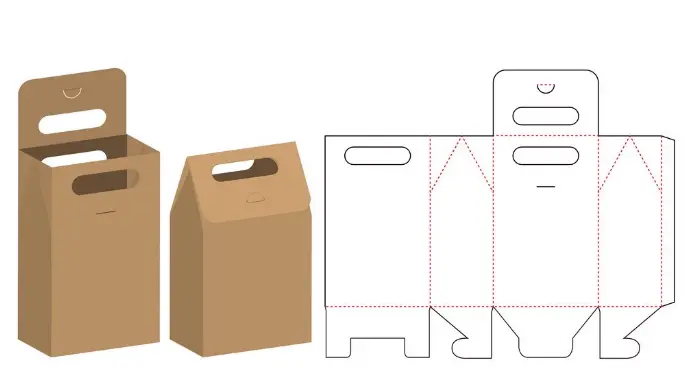
The entire operation starts with a dieline—a digital template that maps every cut path, fold line, and crease. Designers create this outline before any physical die gets made. It defines how a flat sheet becomes a three-dimensional package.
How Die Cutting Works: A Step-by-Step Breakdown
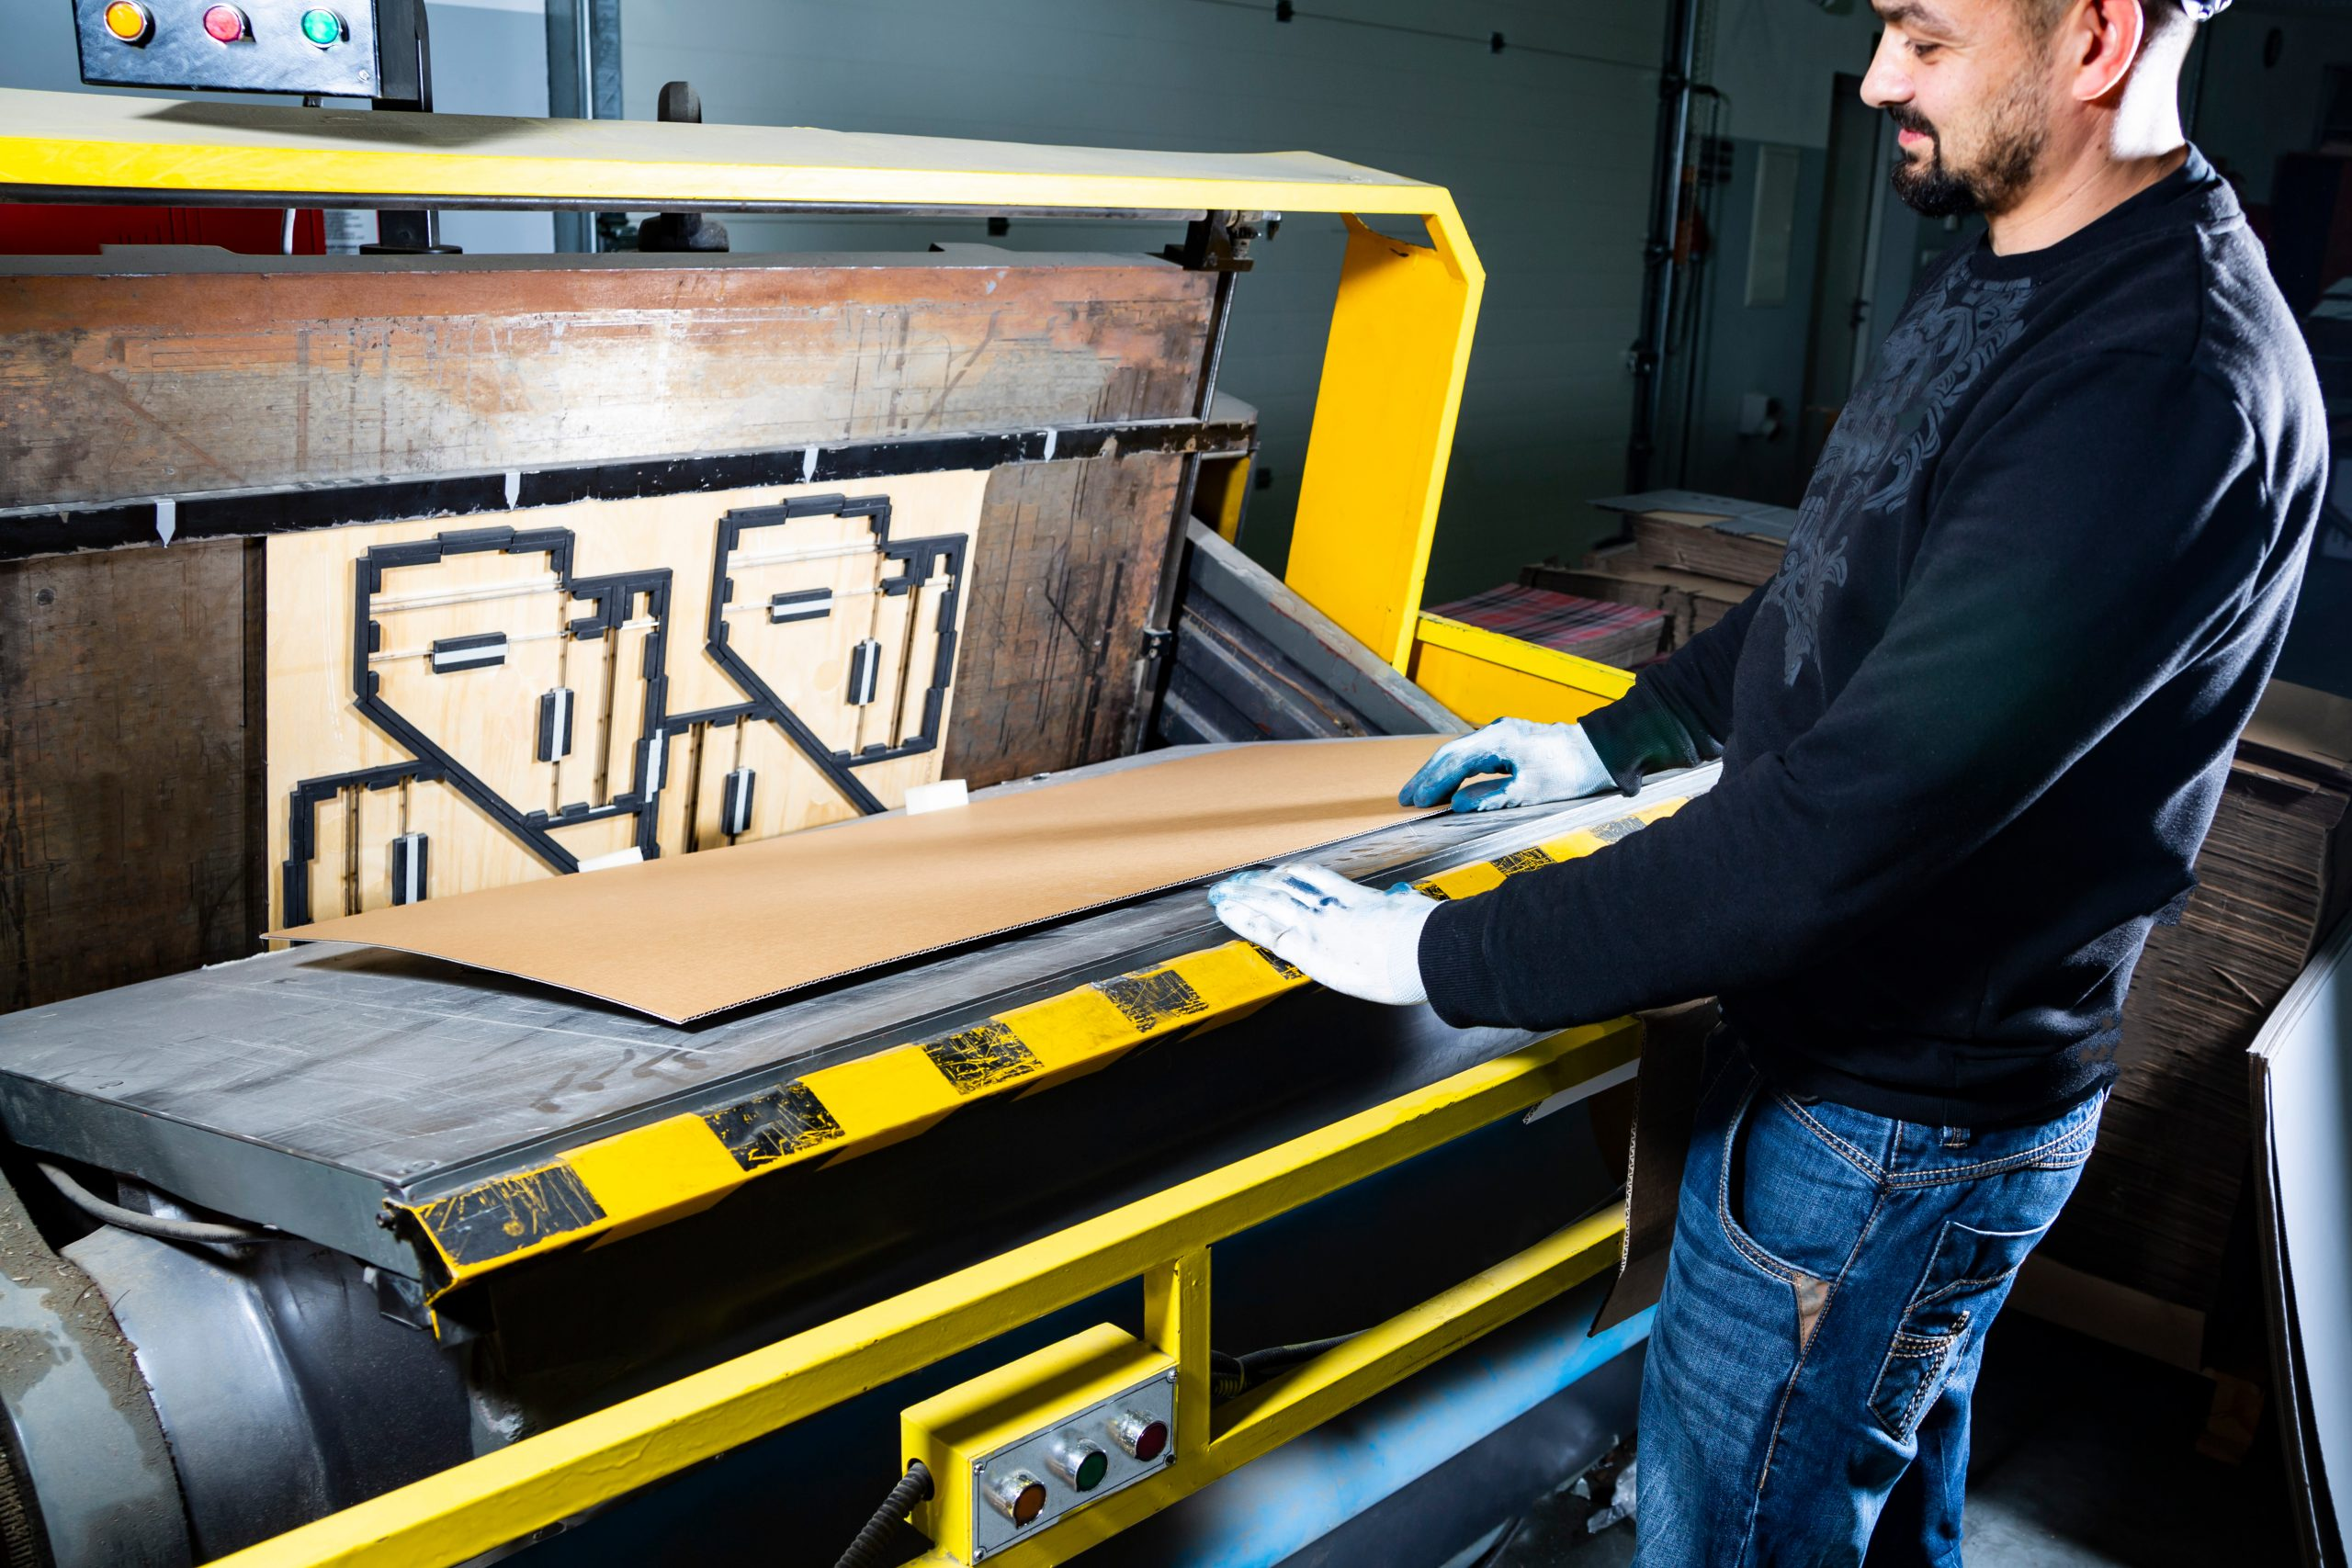
Die cutting looks instant. But it’s actually a planned sequence. It turns raw sheets into precise packaging parts in six stages. You need strict detail at every step. This stops waste and ensures the box folds right.
Step 1: Design Finalization and Die Creation
It starts with the dieline. CAD software creates this digital blueprint. It maps every cut, fold, and glue tab. You translate a 3D box idea into a flat 2D pattern.
Lock the design, then build the physical die. Think of it as a custom industrial “cookie cutter.” We hammer sharpened steel rules into a laser-cut hardwood base. Different blades handle different tasks:
-
Cutting Rules: Sharp blades slice right through the material to define edges.
-
Creasing Rules: Blunt, rounded edges press the fiber. This creates a fold line (hinge) without cutting.
-
Perforating Rules: Notched blades leave small gaps. These work perfectly for tear-away strips.
Step 2: Material Preparation
Bad material means bad cuts. So preparation counts. Operators cut stock rolls or sheets to the exact feed size. But the real work happens during inspection.
The team checks for issues before starting the machine. Missing these could ruin the run:
-
Flatness: Even small warps cause misalignment.
-
Grain Direction: Watch the grain for folding. Cut against it wrong, and the box cracks when you fold it.
-
Surface Cleanliness: Dust effectively stops the die from a clean cut. This hurts adhesive labels most.
Step 3: Machine Setup (The “Make-Ready”)
Here, operator skill shines. You don’t just press “Start.” Mount the die, then run the “make-ready” process.
Operators align the registration to match the print. They keep tolerance tight, just ±0.5mm. Then they calibrate pressure. Too little pressure? The box won’t punch out. Too much? You crush the cardboard flutes. Run a test on scrap material to dial this in. Ensure creases are deep enough to fold, but don’t tear the liner.
Step 4: The Cut
Now for the moment of truth. Flatbed or rotary machine, the physics don’t change. Huge, controlled pressure drives steel rules into the material.
In a split second, three things happen at once:
-
The cutting blades cut the shape from the sheet.
-
The creasing rules press fibers to make fold lines.
-
Rubber ejectors (foam blocks on the die) compress during the cut. They spring back fast. This pops the material off the blades so it doesn’t jam.
Step 5: Stripping the Waste
The cut is done. But the piece still hangs onto the waste material, or “skeleton.” You need to remove this excess.
High-speed commercial runs handle this on their own. Mechanical fingers or air blasts knock away scraps. Complex designs with tiny holes (like hang tags) might need manual stripping. Efficient factories send waste straight to recycling pulpers.
Step 6: Quality Control & Finishing
Boxes pass a final check before gluing or shipping. Quality control goes beyond looks. It ensures functionality.
-
Dimensional Accuracy: Stick to the CAD file measurements.
-
Crease Integrity: Will the box fold square? Or does it lean?
-
Clean Edges: Check for “hairs” or rough spots on heavy cuts.
Pass these checks. Then the blanks move to folder-gluer machines. Finally, they become finished boxes.
Types of Die Cutting Methods: Finding Your Fit
Not all packaging is created equal, and neither are the machines that cut them. The choice between flatbed, rotary, and laser isn’t just about preference—it’s a calculation based on volume, material thickness, and budget.
Flatbed Die Cutting
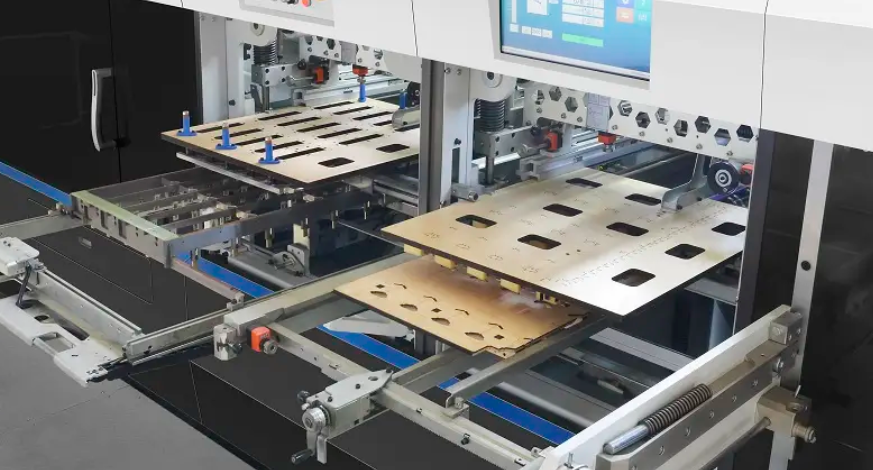
Think of flatbed die cutting as a giant industrial stamp. A flat steel rule die is pressed vertically down onto the material sheet. Because the material remains stationary during the cut, this method offers superior accuracy for intricate designs.
The Trade-off: It’s a stop-and-go process. The machine must pause to feed each sheet, which limits speed to roughly 3,000–8,000 sheets per hour. While slower, it is the king of versatility, handling everything from thick 3mm rigid board to delicate labels without crushing them.
Best For: Short to medium runs (500–20k units), luxury packaging requiring tight tolerances, and thicker materials.
Rotary Die Cutting
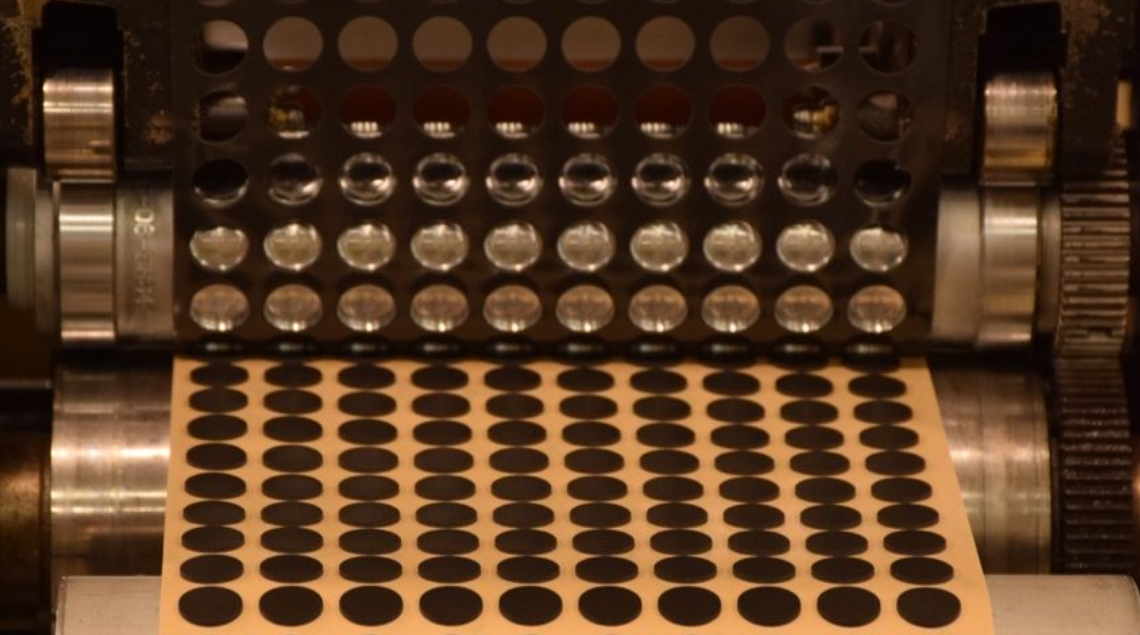
If flatbed is a stamp, rotary die cutting is a rolling pin. The cutting blades are curved around a cylindrical die that rotates continuously against a hardened anvil roll. The material is fed as a continuous web (roll) rather than sheets.
The Trade-off: Speed is the main advantage here. These systems can process 100–200 linear meters per minute—perfect for high-volume corrugated boxes or millions of labels. However, the tooling is expensive (cylindrical dies cost significantly more to manufacture), and the curved nature of the die makes it less suitable for ultra-thick materials or extremely fine details.
Best For: Mass production (50k+ units), standard shipping boxes or roll labels, and simple repeating shapes where low unit cost is the priority.
Laser Die Cutting

Laser die cutting ditches physical tools entirely. A high-speed laser beam burns or vaporizes the material along a digital path commanded by a computer. It is the ultimate tool for prototyping and intricate, lace-like designs that would break a steel blade.
The Trade-off: It offers zero setup time—you can change a design file and start cutting in seconds. But it is slow, often running at just 1–2 meters per minute for detailed work. Plus, the heat can leave burnt edges on certain materials, and it lacks the ability to create physical creases (it can only score/cut).
Best For: Prototypes, ultra-short runs (under 500 units), and intricate patterns impossible to achieve with steel rules.
Comparison at a Glance
Use this framework to decide which method suits your current project:
|
Feature |
Flatbed |
Rotary |
Laser |
|---|---|---|---|
|
Ideal Speed |
Medium (3k-8k/hr) |
High (fast continuous web) |
Low (precision focused) |
|
Tooling Cost |
Moderate ($200-$800) |
High ($1,500-$5,000) |
Zero (No physical die) |
|
Precision |
High (Best for detail) |
Standard |
Ultra-High |
|
Setup Time |
Hours |
Hours |
Minutes |
Die Cutting Materials: Pick the Right Foundation
Your packaging performance depends on your material choice. Think of it as a canvas. Too weak? The box collapses. Too thick? You won’t get clean cuts. Here are the four main options and how they impact cutting.
Paperboard: The Retail Standard
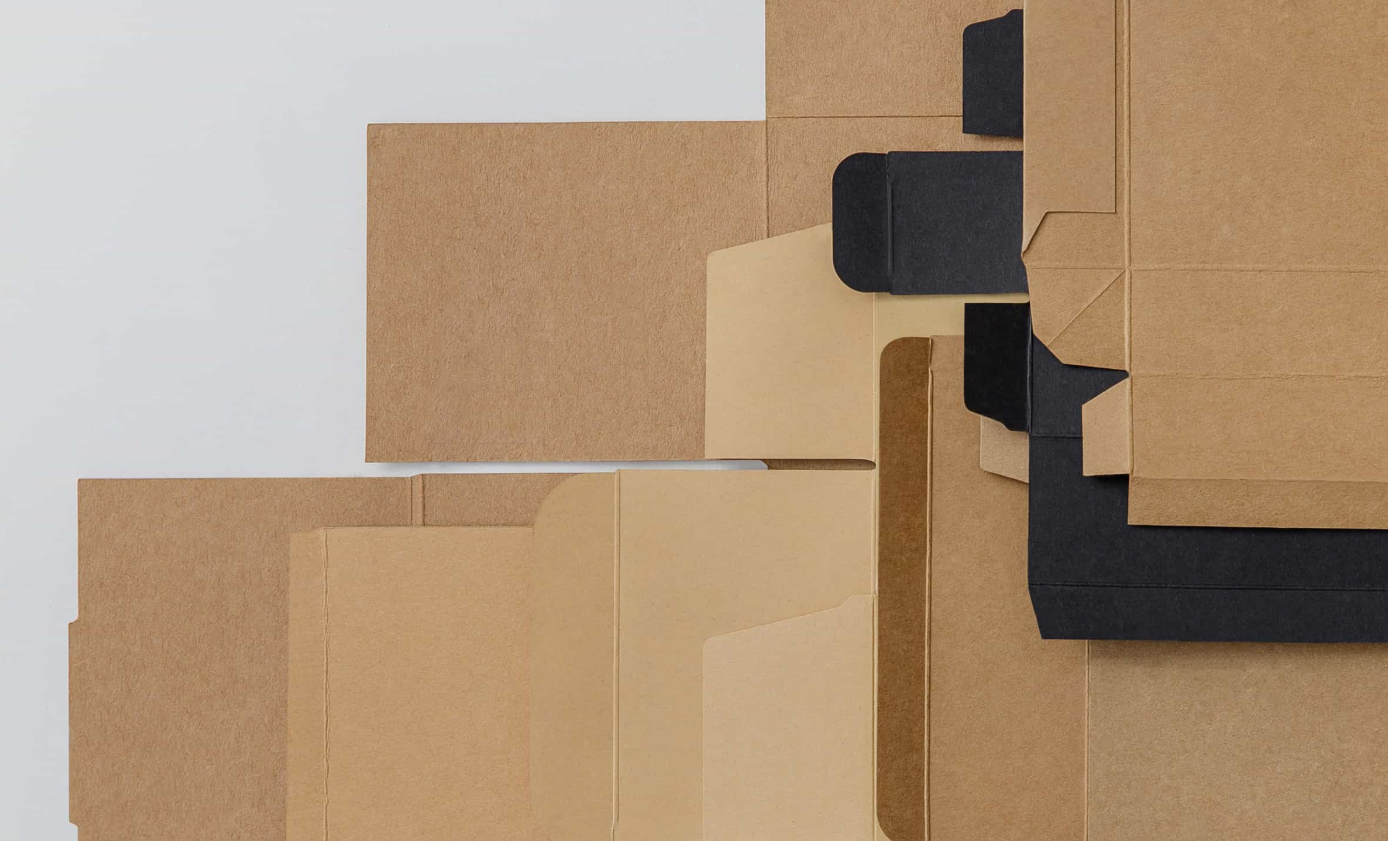
You see this on cereal boxes, cosmetics, and medicine cabinets. It acts like thick paper—smooth, printable, and easy to fold.
Best For: High-quality printing, retail shelves, and lightweight products.
Why It Works: The smooth surface works perfectly for logos and vibrant colors. It handles intricate details, like window cutouts, very well.
The Watch-Out: Watch out for “Delamination.” Too much cutting pressure makes the paper layers split. They separate like page corners in an old book, leaving rough edges.
Corrugated Cardboard: The Shipping Hero
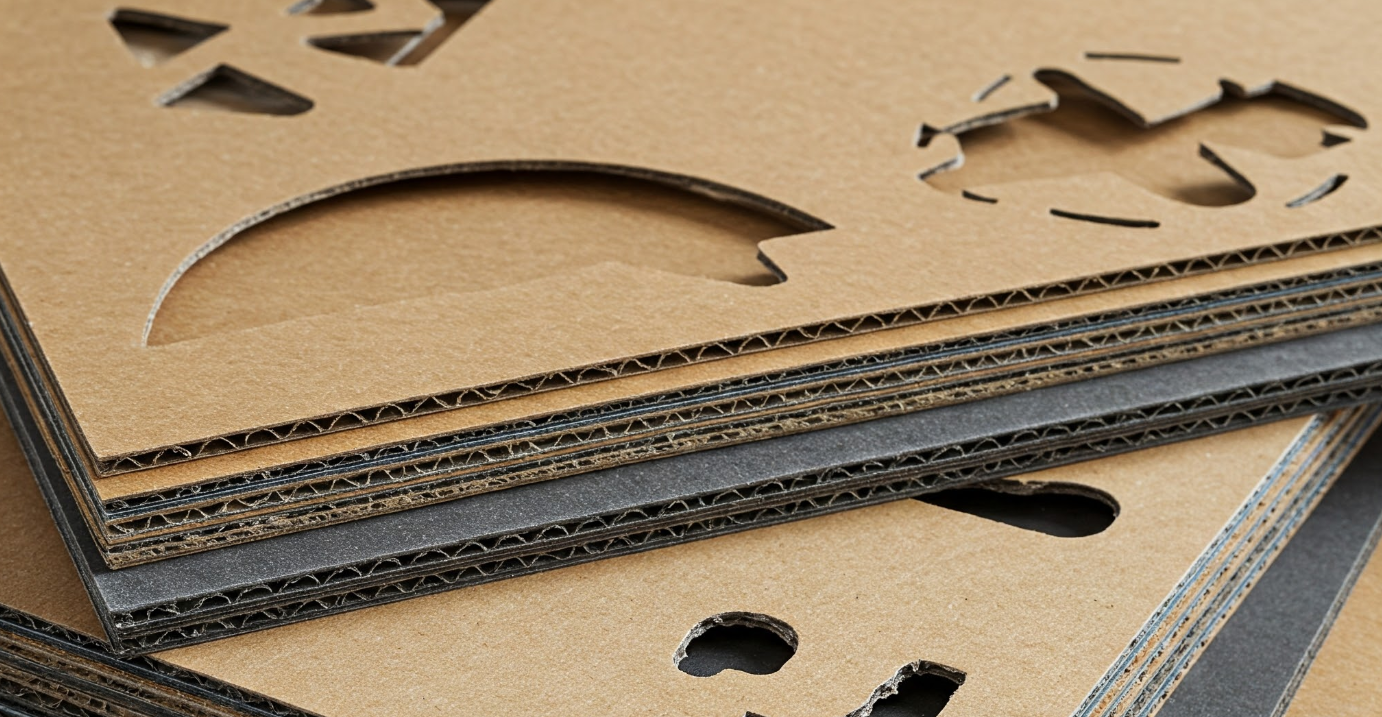
Corrugated acts like an engineering marvel. It’s a “sandwich” with a wavy center (flute) between two flat liners. This air cushion keeps your goods safe during shipping.
Choosing Your “Flute” (Thickness):
-
E-Flute (Thin): Looks flat. Great for pizza boxes and high-quality printing.
-
B-Flute (Medium): The all-rounder. Fits retail displays and counter-top boxes.
-
C-Flute (Thick): The standard shipping box. Offers max cushion, but printing looks less sharp.
The Challenge: You must cut the material without crushing the wavy center. Heavy die pressure flattens the flute. Then, the box loses its structural strength.
Rigid Stock: The Luxury Feel

Common for iPhone boxes, jewelry cases, and board games. This material stays rigid and doesn’t fold. The weight and stiffness show off premium quality directly.
Best For: Luxury goods, keepsake packaging, and heavy items.
The Challenge: It’s tough. Standard machines struggle to get clean cuts on 2mm+ boards. You need heavy-duty industrial presses (often hydraulic) to slice through. This prevents bending the blade or the board.
Plastics & Foam: The Specialty Players
Sometimes paper isn’t enough. You might need a clear plastic window or a foam insert to hold a camera lens.
The “Bounce” Factor: Unlike paper, plastic and foam are elastic. Blades hit them, they compress, then they “spring back.”
The Fix: This often needs Rotary Die Cutting. Ejectors push the material out. Or try Laser Cutting to melt through the material for a clean edge without physical pressure.
Advantages of Die Cutting for Custom Packaging
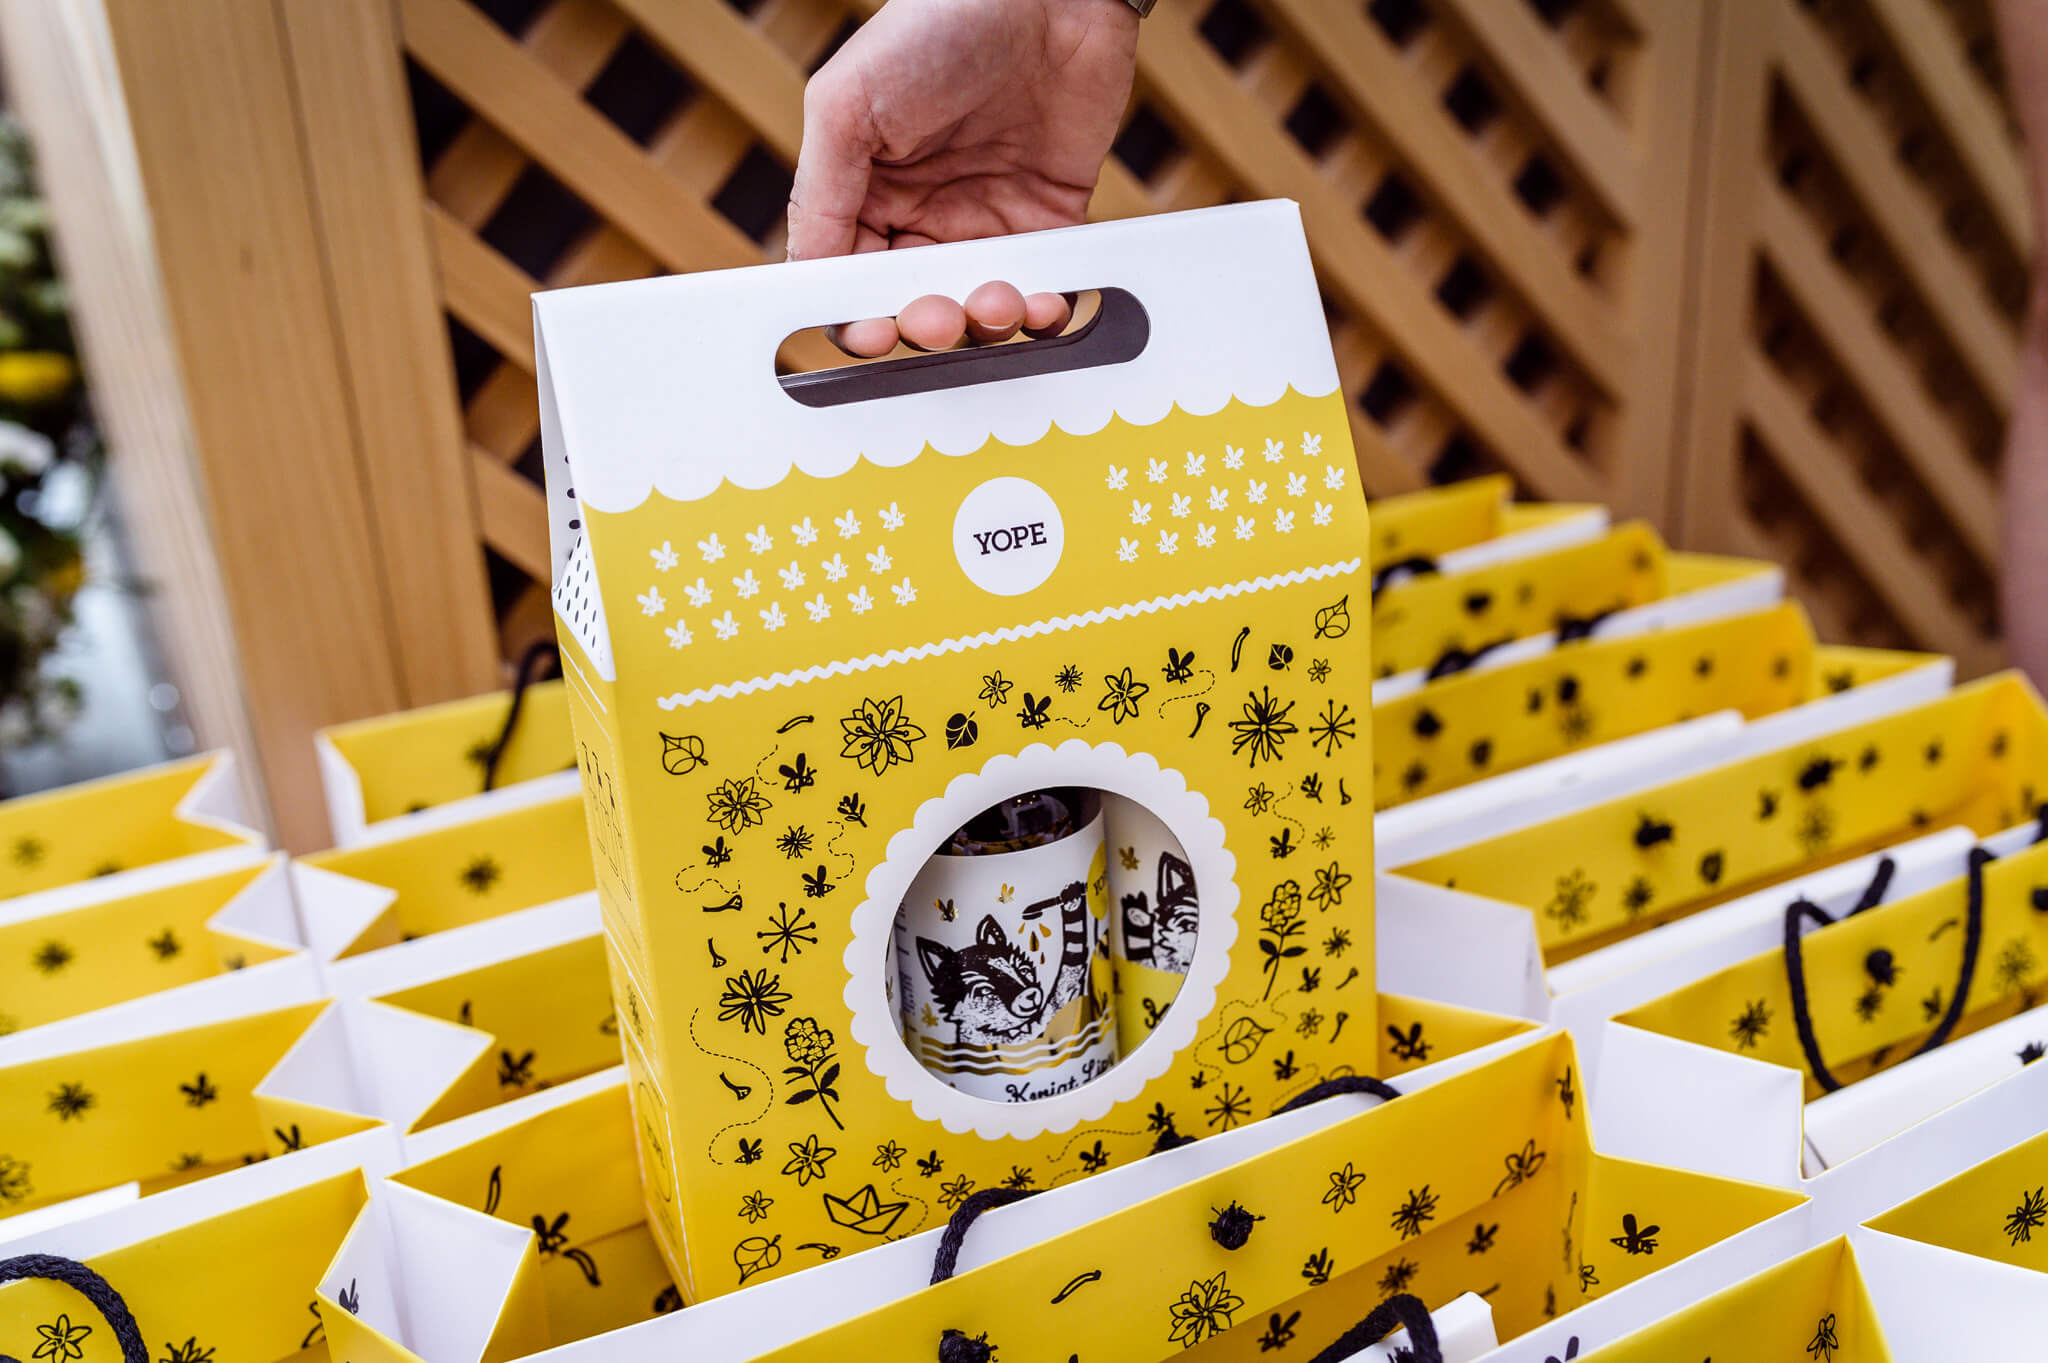
Die cutting is not just a packaging manufacturing step. It is a key asset. It sets pros apart from amateurs. Precision die cutting affects your bottom line. You might be a startup scaling a product. Or you might manage logistics for global fulfillment. In either case, this matters.
Design Freedom: End the “Sea of Sameness”
Retail aisles are full of boring rectangular boxes. Die cutting breaks that monotony. You can move past standard shapes. Create structures that match your product’s curves. Tell a visual story. We mean more than just the outer outline. Techniques like kiss cutting create detailed windows. These show your product’s texture but keep the product packaging strong. Add pop-up mechanisms or magnetic closures to the design. This creates an unboxing experience. Customers will remember it long after the box is gone.
Speed & Scalability: Stop Production Bottlenecks
Digital cutting tables cause delays on large orders. Die cutting solves this problem. The process changes from a slow trace to an instant stamp. A rotary setup produces 50,000 to 80,000 folding cartons in one shift. The tool cuts, creases, and perforates all at once. It happens in a split second. You can handle viral trends or holiday rushes. Your supply chain stays stress-free.
Cost Efficiency: The Volume Advantage
Many think custom dies cost too much. Upfront tooling fees of $200 to $5,000 might seem like a hurdle. But the math changes with volume. For a 100,000-unit run, the cost drops to fractions of a penny per box. The speed cuts your per-unit cost by almost half. Also, professional nesting tools use every inch of your material. This precision cuts waste to just 5-10%. Manual methods often waste 20% or more. You save money and material.
Functional Precision: End Assembly Nightmares
Customers hate tear strips that don’t tear. Production lines stop when box tabs won’t lock. Die cutting prevents these failures. It offers consistent results. Tolerances stay tight at ±0.3mm. Every locking tab snaps into place. Automated case erectors need this precision. Even a small bend can jam the line. Precision perforation also makes “easy-open” features work well. This protects your product and keeps customers happy.
Going Green: Efficiency Counts
Being eco-friendly takes more than recycled paper. It requires efficiency. Die cutting supports “right-sizing.” You build the box around the product. You avoid filling big boxes with plastic packing. A tighter fit lets you stack about 20% more units on a pallet. Fewer pallets put fewer trucks on the road. This lowers your carbon footprint. It helps your operations run better. Also, waste material separates cleanly during stripping. Recycling scrap paper becomes easy.
How to Choose a Die Cutting Partner
Picking a packaging supplier isn’t just about comparing price tags. It’s about finding a partner who won’t disappear when a deadline gets tight. The wrong choice leads to delayed shipments and boxes that fall apart. Here is how to vet potential providers and spot red flags before you sign a contract.
Start with Your Volume, Not Just the Design
Before you send a single email, be clear about your numbers. This is the first filter. If you need 500,000 shipping boxes, you need a factory equipped with high-speed rotary die cutting gear. If you approach a smaller shop that only has flatbed machines, they might take the job but outsource it (charging you a markup) or clog their production line, missing your deadline. Be honest about your scale upfront. It saves everyone time.
Dig Deeper into Technical Capabilities
Don’t just ask, “Can you do this?” Most sales reps will say yes. Instead, ask specific questions about their equipment. For example, if you are using corrugated board, ask how they handle flute crushing. A capable provider will explain their pressure calibration or use of specific rubber ejectors. If you need intricate labels, ask about their kiss cutting tolerances. You want to hear numbers (like ±0.3mm), not vague promises of “high quality.” Also, ask about their scrap rates. Efficient shops keep waste below 8%; if they don’t know their scrap rate, they probably aren’t managing costs well.
The Truth About Tooling Costs
Pricing is often utilized to hide inefficiencies. A transparent quote should clearly separate the one-time tooling fee (the cost of the physical die) from the per-unit manufacturing cost. Flatbed dies might cost a few hundred dollars, while rotary cylinders can run into the thousands. If a provider rolls this into a single “all-in” unit price, be careful. That makes it hard for you to see volume discounts later on. You want clarity: pay for the die once, and own it.
Verify with Physical Proof
Website photos can be staged. Physical samples don’t lie. Ask for samples from previous runs that are similar to your project. Don’t just look at the print quality; look at the cuts. Are the edges clean or fuzzy? Do the extensive crease lines crack the paper? If they claim to be sustainable, check for certifications like FSC right on the sample. Furthermore, ask for references. A quick call to a current client can reveal how the shop handles crisis moments—because that’s when you really need a packaging partner, not just a vendor.
The “Pilot Run” Safety Net
Never commit to a 100,000-unit order on day one. Insist on a pilot run—maybe 1,000 to 5,000 units. Yes, the unit cost will be higher, but think of it as insurance. This test reveals communication gaps and quality issues while the stakes are low. If the tabs don’t lock perfectly or the shipping boxes crush on a truck, you can tweak the die design cheaply. If a provider fights you on doing a pilot run, take it as a warning sign.
Ready to Elevate Your Packaging? Let’s Talk.
Understanding the die cutting process is the first step. Finding a partner who can execute it flawlessly is the second. You don’t need just a vendor who owns a machine; you need a team that understands the nuance of your brand.
At CNNBox, we bridge the gap between creative design and industrial precision. We have refined our tooling and techniques to handle the specific challenges of different materials. Whether you are looking for intricate, kiss-cut labels and stickers that peel perfectly, structural paper boxes that snap shut with a satisfying click, or premium paper bags that carry your brand’s weight, we deliver consistency.
Don’t let rough edges or poor folds compromise your product’s first impression. Let us show you what professional die cutting looks like.
Have a design in mind? Reach out to the CNNBox team today. Let’s review your dieline, pick the right material, and bring your vision to life.


