
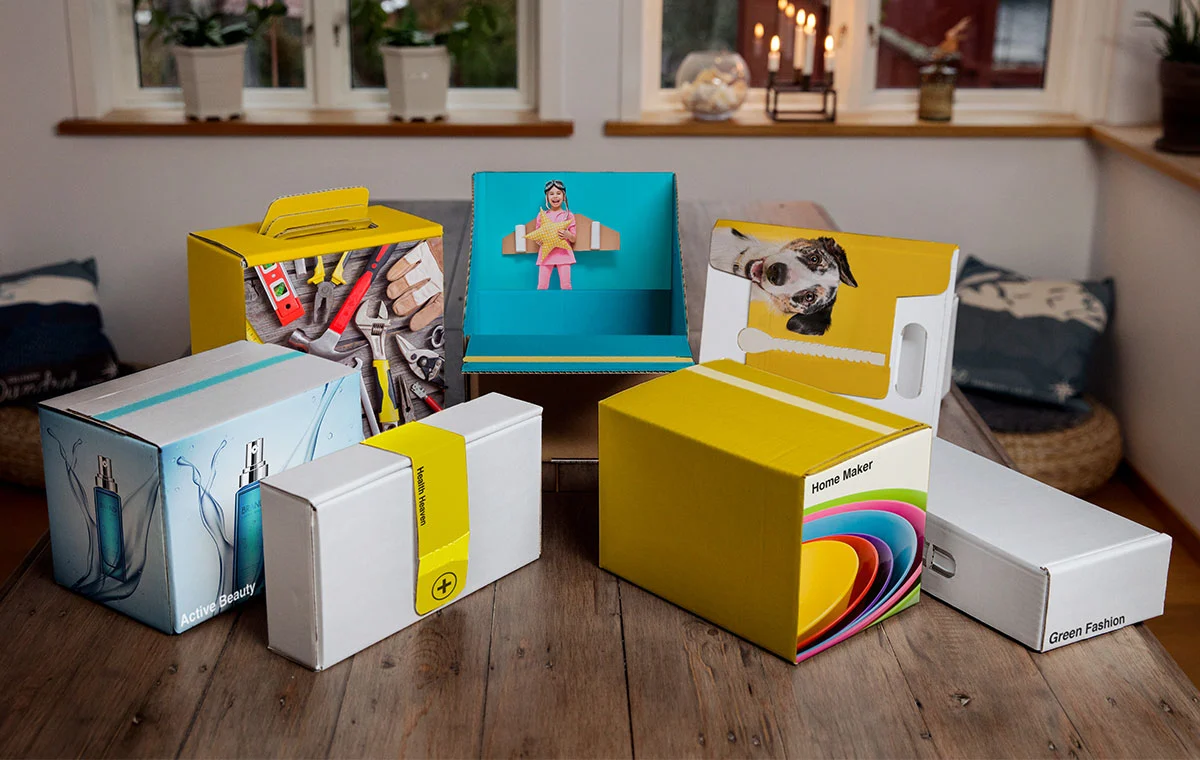
Digital printing on corrugated boxes transfers digital images onto corrugated board surfaces. No printing plates needed. The technology cuts out traditional setup steps. Short-run production now makes financial sense for the first time in packaging history. Now brands and packaging producers face a key choice: how to use digital printing without losing quality or profit on corrugated materials.
The real challenge goes beyond buying new equipment. You need to understand how digital inks work with corrugated board. Design strategies matter too. This knowledge separates okay results from great, shelf-ready packaging.
Are you looking at inkjet printing systems for short runs? Or maybe you’re improving your direct-to-board process. Either way, five core techniques can save you time and money. They help you avoid expensive mistakes and get production right from the start.
These strategies tackle the problems that kill most digital printing projects. Artwork files don’t match system requirements. Ink won’t stick to the board surface. File prep creates bottlenecks. Equipment sits out of alignment. Quality control fails, and you end up with rejected orders and missed deadlines.
Tip 1: Optimize Artwork Design for Corrugated Substrate Texture
Corrugated board is a beast of its own. Unlike flat paperboard, it has a complex structural “sandwich” underneath the printing surface. That wavy flute structure creates an uneven landscape of peaks and valleys. If you treat it like standard paper, your ink will spread, fine details will blur, and your barcodes might not scan.
To get shelf-ready results, you need to understand how the substrate fights your design—and how to win that battle before you even turn on the press.
Understanding Board Texture and Dot Gain
The texture of the board impacts print quality in ways you can measure. On standard single-wall boards, you often face dot gain of up to 20-30%. Essentially, ink hits the high points of the flute first and then spreads into the lower valleys. This means graphics will look darker and “fatter” than they do on your monitor.
Fine lines are the biggest casualty. Any line thinner than 0.2mm risks getting distorted by the board’s undulation (the “washboard” effect). Your artwork needs to be robust enough to survive this texture.
Design Defenses: How to Compensate
Don’t wait for the press operator to fix this. Build these compensations into your design file:
- Stick to Vector: Use AI or EPS formats as your foundation. Raster images (pixels) struggle to adapt to substrate variations without losing edge definition. Vector lines stay sharp.
- Beef Up Your Lines: Set a strict minimum line thickness of 0.25-0.5mm. If you are printing on B-flute (which has wider gaps), bump that thickness up by 1.5x. Thicker lines bridge the gaps between flutes significantly better.
- Smart Trapping: Corrugated board flexes during transport through the press. To prevent white gaps from appearing between colors if the registration shifts slightly, apply a 10-15% trap where colors overlap. It’s your safety net.
Matching Resolution to Flute Type
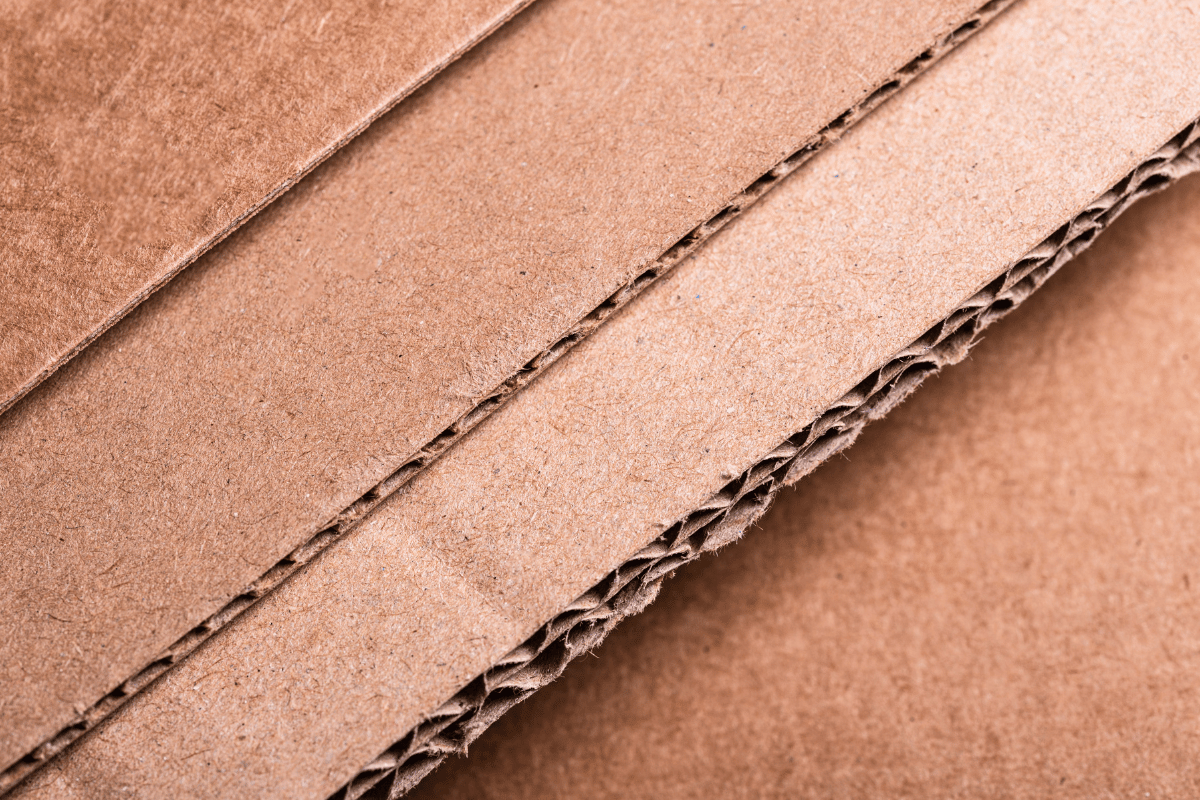
Not all cardboard is created equal. Your design limitations depend heavily on the specific flute profile you are running:
E-Flute (Microflute, ~1.6mm):
This is the premium choice for high-quality retail packaging. The tighter flute pattern creates a smoother surface, allowing for finer detail. You can push resolution to 85-100 LPI and use font sizes as small as 6 points. Just remember to keep a 3mm safety margin from fold lines.
B-Flute (Standard, ~2.5mm):
This is the workhorse of the shipping world (holding about 65% market share). It requires more caution. Drop your resolution to 65-80 LPI and increase minimum fonts to 8 points. Because the valleys are deeper, you need a larger safety margin—aim for 5mm to be safe.
The “Real World” Proofing Protocol
Simulation isn’t enough. Since digital presses allow for short runs, print a physical proof on the actual target flute.
When inspecting the proof, look past the colors. Check the edge clarity at full production speed (around 250m/min). Sometimes a design looks great when the machine is crawling but falls apart at speed. Also, check your gradients. If you see banding, reduce ink coverage by 8-10% or use vector patterns to smooth the transition. Digital ink on corrugated board behaves differently than on coated stock; your proof is the only way to catch these surprises early.
By optimizing your files for the physical reality of corrugated board, you prevent the vast majority of quality issues downstream.
Tip 2: Select Compatible Inks and Master White Ink Application
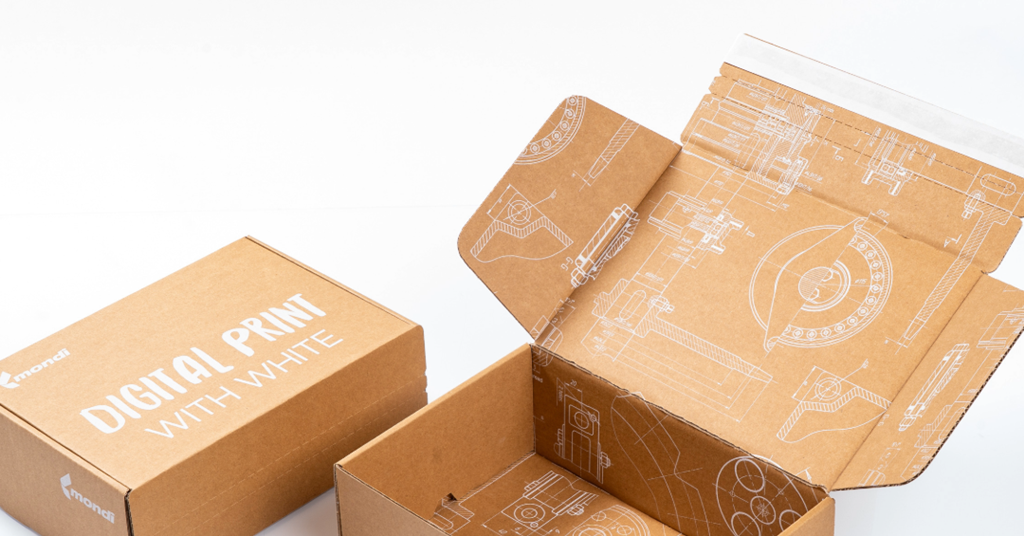
White ink separates pro-level corrugated packaging from amateur work. You get the opacity needed for dark materials. Plus, colors pop on uncoated board. But be careful. Poor management of this specific channel starts most production failures.
Managing White Ink Costs
Getting the right opacity takes 3 times more ink volume than standard CMYK colors. This hits production costs hard. You must budget with precision. Ignore this multiplier, and your profit margins vanish.
You have two main application strategies:
- Spot application: Cover specific areas. This works perfectly for logos or text on dark or metallic materials. It saves you money.
- Flood coverage: Create a full undercoat across the print area. You use more volume—often double a standard color layer. But the quality jump on rough corrugated surfaces is undeniable.
Black and clear substrates are popular now. Demand for high-opacity printing surged by 30% recently. Look at flexible packaging. White ink accounts for 50% of total ink spending there. Corrugated markets follow this same trend.
Preventing Sedimentation and Clogs
Titanium dioxide pigments give white ink its brightness. They are heavy and settle fast. Keep them moving. Otherwise, you face printhead clogs and poor print quality.
Recirculation keeps things flowing. Roland systems start auto-circulation after about 6 hours idle. HP Latex platforms often run continuous recirculation through the printheads. Your equipment lacks these features? Intervene manually. Stir ink tanks every 4 hours during shifts. Set a reminder. Stick to it.
Also, check your pack size. Smaller 1-liter pouches let you refresh supply often. You lower the risk of expiration or settling compared to larger cartridges.
Application Techniques for Corrugated Board
Corrugated board is thirsty. It soaks up ink fast compared to rigid substrates. Standard settings often give you dull, washed-out images.
Use higher volume settings or specialized engraving patterns (like elongated cell HVP). Push more fluid into the fiber structure. You get proper optical density even at high speeds. Always test opacity on the actual stock. Absorption rates shift between coated and uncoated linerboard. A design might look brilliant on one but disappear on the other.
Pick the right chemistry:
- UV-curable inks: Great for sharp detail. But they clog without active maintenance. Use them for high-end, smooth finishes.
- Latex inks: You get high opacity (up to 91%) and easier maintenance. They are often food-safe. This makes them a smart choice for food packaging.
Actionable Steps for Consistent Results
Keep your white ink process profitable with this workflow:
Test Before You Run: Make reference samples with 1, 2, and 3 layers of white. Find the minimum coverage for your quality standard. Two layers work? Don’t waste ink on a third.
Track Consumption: Monitor usage per channel via print management software. Check the true cost of that white underbase. You might need to adjust your pricing model.
Price Specifically: Quote jobs with a “White Ink Multiplier.” Never treat a flood-white job like a CMYK-only job.
Maintain Discipline: Brief operators on the machine’s recirculation needs. A five-minute routine saves hours of downtime later.
Tip 3: Speed Up Setup with Smart Digital File Prep
File prep bottlenecks kill printing efficiency silently. Your press might run thousands of boxes an hour. But that speed means nothing if your pre-press team gets stuck fixing artwork all day. Studies show knowledge workers waste nearly 20% of their time just searching for and organizing data. This hidden cost adds up fast in a print shop. It often costs more than press downtime.
Digital corrugated printing removes physical plates. So, your setup time is purely digital. Streamline this process. You unlock the true “on-demand” potential of your equipment.
Standardizing File Formats
Client-printer back-and-forth kills margins. Do not just accept “whatever the client sends.” Establish a strict “Golden Master” file protocol.
Forget native design files. Demand PDF/X-4 formats for all jobs. PDF/X locks in fonts and keeps color spaces right. It stops layout shifts common between Illustrator versions. You get the stability you need.
Also, fix your color mode before the file hits the RIP. Leaving RGB graphics? Your RIP software must convert them instantly. This adds calculation time to every job. You lose 15-30 minutes per batch. Force a CMYK + Spot Channel workflow early. This keeps the press running smooth.
Automate Repetitive Tasks
Is your team checking bleeds or fold lines by hand? That slows you down. Document automation cuts processing time by 70%.
Use hot folders and pre-flight software. Let the computer do the boring work. It checks document sizes against die-lines. It verifies fonts and flattens transparencies. Your skilled operators can then focus on creative color correction. They solve complex packaging structural issues instead of basic file hygiene.
Choosing the Right Workflow
Digital printing is flexible. But feeding the machine matters. Try this dual approach:
- Large, seasonal campaigns: Use batch processing. Queue hundreds of SKU variations at night. The RIP works while the shop is closed. You walk in to a “ready-to-print” queue in the morning.
- Rush prototypes: Use a real-time CDC (Change Data Capture) workflow. Drop a file and get an instant error report. Fix it. Print it. All within minutes.
Clean Up Your Transfer Pipeline
File movement speed matters. We’ve seen shops push terabytes through old networks. It creates a digital traffic jam.
Clean up your files. Use lossless compression. You shrink file sizes by 60-80% without hurting image quality. Bloated files don’t print better. They just load slower. Modern cloud-based submission platforms beat physical USB drives or FTP sites for speed and traceability. Treat your data pipeline like a physical conveyor belt. Keep it clear. Keep it fast.
Shift focus from “fixing files” to “managing workflows.” You turn your pre-press department into a speed advantage, not a cost center.
Tip 4: Match Your Equipment to Your Actual Production Reality
Selecting the right digital press is the single biggest driver of profitability in corrugated box printing. But here is the trap many fall into: buying based on “spec sheet vanity”—chasing the highest speeds or resolution—rather than matching the machine to your actual business model. If you buy underpowered equipment, you’ll choke during peak seasons; buy too much, and the capital depreciation will eat your margins alive while the machine sits idle.
Instead of getting lost in model numbeflunnrs, think of production volume in four distinct tiers. Each requires a different investment strategy.
Low Volume: Entry-Level Systems
If your primary goal is checking structural design or presenting visible concepts to clients, you seldom need industrial iron. For volumes under 50,000 pages per month, standard commercial laser or advanced desktop inkjet systems are often sufficient. While these units struggle with thick E-flute boards or heavy textures, they allow you to produce “look and feel” mockups on cardstock incredibly cheaply.
The advantage here is the low barrier to entry. You can validate designs and secure client approvals without firing up a main production line. However, be realistic: these are not production machines. If you try to run thousand-unit custom printed box orders on them, the cost of ink cartridges and the wear on the feed mechanisms will destroy any profit you hoped to make.
Mid Volume: Professional Production

This is where most growing packaging converters find themselves—handling between 50,000 and 500,000 pages monthly. At this stage, you need equipment that bridges the gap between office utility and factory floor. You aren’t just printing samples anymore; you are fulfilling short-run orders that need to look professional.
In this tier, prioritize color fidelity and resolution over raw speed. Why? because short-run corrugated boxes are often used for promotional displays or direct-to-consumer packaging, where the viewing distance is close. Your equipment needs to handle variable data and maintain consistent brand colors across a few hundred units. Look for presses that offer automated calibration features, so your operators spend less time tweaking color curves and more time printing.
High Volume: Industrial Presses
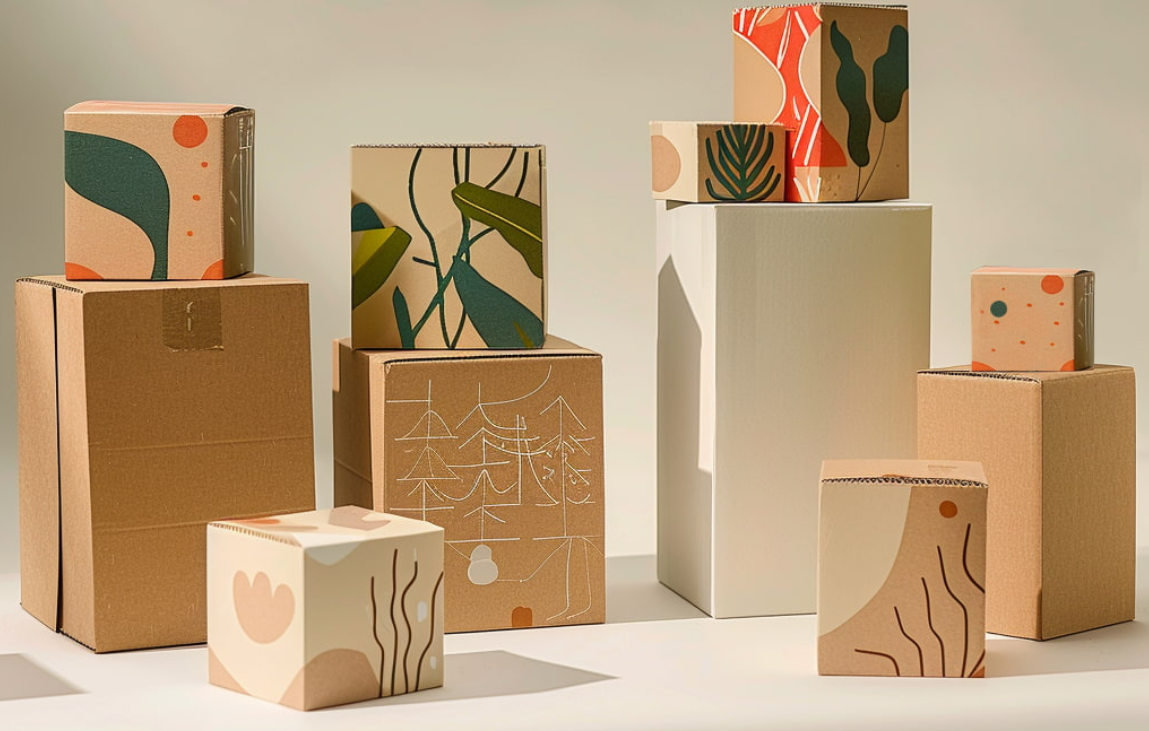
When your operation scales above 500,000 prints per month, the metrics change completely. Speed is important, but uptime is everything. A press rated for 120 pages per minute that jams every hour is far less profitable than a steady 100 ppm machine that runs seamlessly for a full shift.
At this level, robust paper handling becomes your critical feature. Corrugated board is dusty and abrasive; it punishes delicate feed mechanisms. Industrial systems in this category are built like tanks to handle that abuse. Your calculation here should shift to “Total Cost of Ownership.” The upfront price tag matters less than the cost of service contracts and the durability of consumption parts.
Mass Production: Maximum Throughput
For operations pushing millions of pages monthly—think national fulfillment centers or dedicated corrugated packaging lines—you are getting into heavy industrial inkjet territory. Here, the game is strictly about the lowest cost per page. These systems often use tank-based ink delivery rather than cartridges to drive consumable costs down significantly.
Interestingly, some facilities find success not by buying one massive machine, but by deploying “clusters” of mid-to-high tier machines. This offers redundancy; if one unit goes down for maintenance, your entire production capacity doesn’t vanish. Whether you choose a massive single-pass system or a fleet of smaller units depends on your risk tolerance and space.
Calculating Total Cost of Ownership
Don’t let a salesperson sell you capacity you won’t use for three years. Audit your last six months of job tickets. If 80% of your jobs are under 500 units, a massive industrial press is likely overkill. Match the machine to your current reality plus 20% growth, and remember to factor in the hidden costs: maintenance downtime, operator training, and consumable prices. That is how you make digital printing pay off.
Tip 5: Implement a Comprehensive Pre-Print Quality Checklist
Production failures waste more than cardboard. A rejected order kills deadlines, hurts client relationships, and erases profit. Quality control does not start when ink hits the board. It starts when you create the job ticket.
Don’t rely on memory. Successful shops use a structured “Pre-Flight Safety Net.” This catches errors when they cost pennies to fix. Wait too long, and they cost hundreds.
The Four-Level Inspection Framework
Stop scanning files at random. Check them in layers. This system stops errors from slipping through the cracks:
Level 1: Technical Integrity
Focus on file health. Match the file to the “Golden Master” standards from Tip 3. Are fonts corrupt? Is the color profile right for your press? File error in the RIP? Stop immediately.
Level 2: Structural Fit
Check the design constraints from Tip 1. Do bleed areas cover flute shifts? Respect safe zones. This isn’t about art. It is mechanical reality. Logo on a fold line? Flag it now.
Level 3: Material Compatibility
Match your ink strategy to the board type. As Tip 2 showed, uncoated boards drink ink. Are white underbase settings right for the stock’s absorption rate? Also, match the flute type (E-flute vs. B-flute) to the artwork details.
Level 4: Production Parameters
Check the physical setup. Adjust tension settings so you don’t crush delicate micro-flutes. Calibrate drying lamps for the ink density of this specific job.
Combining Software and Manual Checks
You might want to automate everything. Be careful. Automated preflight software works great for Level 1 checks. It finds missing fonts and resolution issues faster than humans. Plus, it flags 90% of technical errors and never gets tired.
But software cannot judge intent. It doesn’t know the client’s brand red looks orange on a shipping box’s kraft board. It cannot see if text is legible on a busy background. So, keep a Manual Visual Inspection for Levels 2 and 3. Use software for math. Use operators for the “feel.”
The “15-Minute” Rule and ROI
Operators often say, “I don’t have time to check.” But you don’t have time not to check. A full review takes an experienced pro about 15-20 minutes per job. Complex designs take 30.
Weigh that investment against the cost of an error. One rejected run of 5,000 boxes wastes material, machine time, and labor. That equals over 100 hours of inspection time. Track your “save rate”—errors caught before printing. You will see this checklist becomes the most profitable tool in your shop.
Continuous Improvement
Make your checklist a living document. A job failed? Ask “Why?” Then add a check item to stop it next time. See adhesion issues often? Add a “Surface Tension Test” to Level 3. Shift your culture. Stop fighting fires. Start preventing them.
Conclusion
Digital printing has changed how businesses handle corrugated packaging solutions. You get flexibility without losing quality. These five essential tips give you the tools to cut production costs by up to 30%. You’ll slash turnaround times in half. Plus, you eliminate the wasteful trial-and-error that comes with traditional printing methods. The tips cover everything from optimizing artwork for substrate texture to using solid pre-print checklists.
The real edge comes from applying these proven techniques across your workflow. Direct-to-board printing technology is just the start. You need to use it right. Producing limited-edition packaging for a product launch? Managing seasonal design variations? These strategies ensure every box delivers the visual impact your brand deserves. Short runs stay profitable too.
Ready to step up your corrugated box printing? Start by checking your current design files against the checklist in Tip 5. Then connect with CNN Box. We’ll help you figure out which technology fits your volume needs. Brands winning shelf space today aren’t spending more on packaging. They’re just printing smarter.


