
Billions of corrugated boxes come off production lines each year. Most share one thing: flexographic printing. But here’s the problem. Packaging newcomers, business owners, and even experienced product managers don’t understand how this technology works. The mechanics stay unclear.
You’re evaluating vendors right now. Maybe considering equipment investments. Or trying to figure out why your supplier demands minimum order quantities. Technical jargon about anilox rollers, printing plates, and ink viscosity leaves you confused.
Understanding flexo printing affects your bottom line. Packaging costs depend on it. So does quality. And your ability to negotiate with suppliers. This guide breaks down the complexity. You’ll learn how water-based inks transfer onto corrugated board. Post-print versus pre-print methods. The key differences that matter.
Launching a product line? Expanding your print shop? Evaluating corrugated box suppliers? You’ll walk away with practical knowledge. The kind that leads to smarter decisions and better results. No engineering degree needed.
What is Flexo Printing
Flexo printing works like a rubber stamp system. Raised plates pick up ink from an anilox roller. This roller is a ceramic cylinder covered in tiny cells. These cells measure exact ink amounts. The plate transfers ink onto corrugated liner board. This solves a key problem: printing on rough surfaces without crushing the flutes underneath.
The numbers show the impact. Corrugated board took over 50% of all global flexo printing volume in 2025. E-commerce drove this growth. Amazon processes over 2 million packages each day in the United States. Each package needs printing. Flexo’s speed and efficiency make this possible.
Real-World Advantages and Honest Limitations
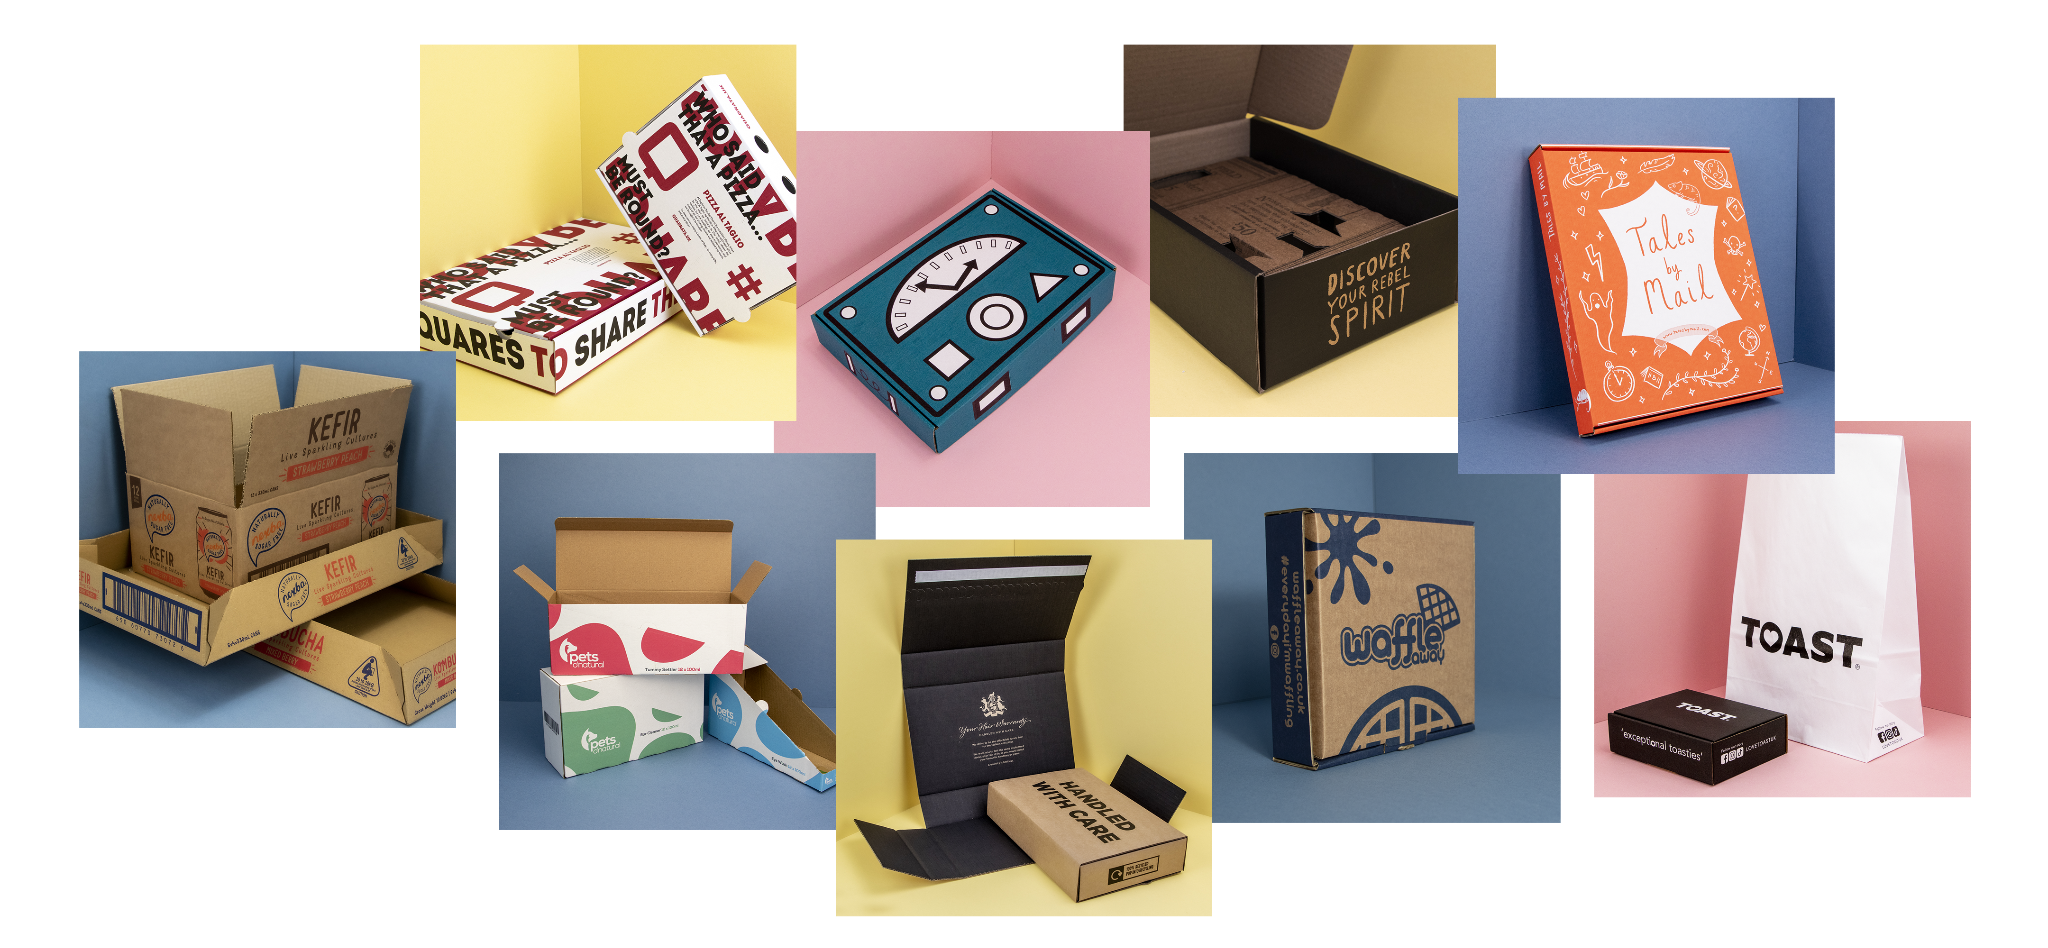
Look at the corrugated box industry. One method dominates the factory floor: flexo printing. Why? Tradition plays a role, sure. But the real drivers are efficiency and scale. Forget the technical specs for a moment. Flexo solves specific business headaches that other methods miss.
Let’s talk about the cost reality. Flexo changes the economics as your order size grows. You have that initial investment in printing plates. We will discuss that shortly. But make those plates once, and they become a long-term asset. Think of it this way. A small batch of 50,000 boxes might cost about $0.15 to $0.25 per unit. Jump that order to half a million. Your per-unit cost drops fast, often to just 8 or 12 cents. Digital printing starts strong on the first box. But it hits a financial wall. It can’t match those savings on high-volume runs.
Then there is the sheer production speed. In logistics, time is inventory. Modern flexo presses are beasts. They churn out 10,000 to 30,000 impressions every hour on pre-print jobs. Print directly onto the corrugated board, and the speeds still leave digital systems behind. A digital press works hard to finish 3,000 boxes. Meanwhile, a flexo line finishes the job, cleans up, and starts the next shift. Shipping worldwide? Need to meet tight delivery windows during peak seasons? This speed difference isn’t just a spec sheet number. It acts as your safety margin.
It also handles almost anything. Corrugated board isn’t a uniform canvas. It feels rough, spongey, and varies a lot. Flexo excels here regarding adaptability. You might print on delicate E-flute for a subscription box. Or perhaps heavy-duty triple-wall paperboard for industrial parts. The process works without crushing the flutes. Plus, eco-conscious consumers demand better options. Water-based flexo inks give you an edge. They look great on recycled paper materials. They also meet food safety standards easily. This gives brand owners peace of mind.
The Limitations You Need to Know
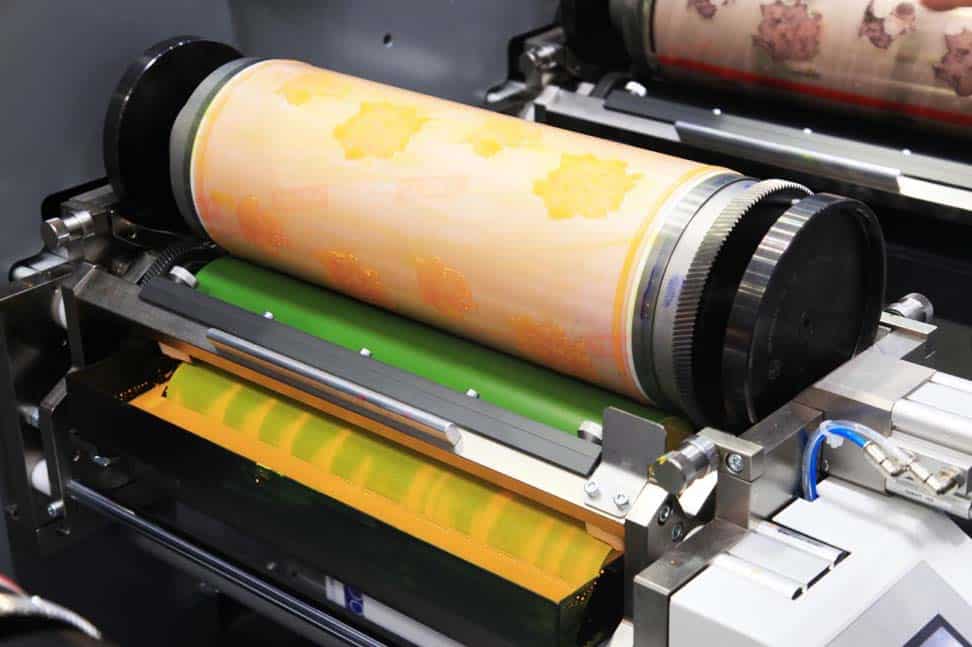
No technology is perfect. We must be honest about where flexo struggles. You don’t want surprises. It is not a magic wand for every single project.
The startup barrier is real. Small businesses testing a new product often find the upfront costs painful. You pay for printing plates. These run a few hundred dollars each. Then add the cost of setup tools like anilox rollers. You might spend over $1,000 in prep before seeing your first printed box. Run a short promo of 500 boxes? The math rarely works out.
Don’t expect magazine-quality photos. Flexo has improved a lot over the years. But physical limits remain. Does your marketing team want a high-gloss 4K photo on a box? Flexo might disappoint them. Fine text and subtle gradients sometimes lose sharpness or fill in. High-end systems push these boundaries, reaching 200 LPI. However, most standard production runs sit in a lower resolution range compared to commercial digital or offset printing.
Registration can be tricky. Remember, corrugated board functions like a paper sandwich with air in the middle. It compresses. The board moves through the press at high speeds and can shift. Colors might not line up every time. We call this registration drift. It happens more often on lightweight boards that warp. Industry standards allow for a few millimeters of wiggle room (±2-3mm). Premium brands demanding absolute precision must pay extra for tighter controls.
Finally, consider your base color. Printing on standard brown craft board resembles painting on a brown canvas. Want bright, popping neon colors? You often need a solid layer of white ink first. This adds another step to the process. It consumes much more ink. This drives up the cost and production time by a noticeable margin—sometimes up to 60%.
Corrugated Box Applications: Flexo Printing Uses
Flexo printing captures 36.8% of global corrugated output volume. That’s billions of boxes across three main categories: e-commerce shipping, retail displays, and industrial packaging. Each category needs different specs. Your application type shows if flexo gives you the best value.
E-Commerce Shipping Boxes: Flexo Leads Here

Amazon processes over 2 million US packages each day. Most arrive in custom-sized corrugated boxes printed via flexo. Why? The tech handles high-porosity liners on micro-flute boards. No crushing of the structure. You get bold graphics on lightweight E-flute (1.5mm). This cuts pallet weight by 20-30%. Lower weight means less shipping emissions.
E-commerce print needs differ from traditional retail. Product details, logos, and barcodes print on brown corrugated. High-line-screen anilox rollers deliver the contrast needed for scannable barcodes at distribution centers. Some brands add inside-print graphics for unboxing experiences. Water-based inks provide the baseline chemistry. They dry fast between stations. They meet recycled-content rules from EU Circular Economy laws.
Cost economics favor flexo here. Job changeover takes under 5 minutes on digital-hybrid presses for orders below 5,000 linear meters. Above that threshold? Dedicated flexo lines deliver the lowest per-unit pricing. FSC and PEFC certification opens access to retailer green-label programs. Major logistics firms want these certifications.
Retail Displays and Point-of-Sale Packaging
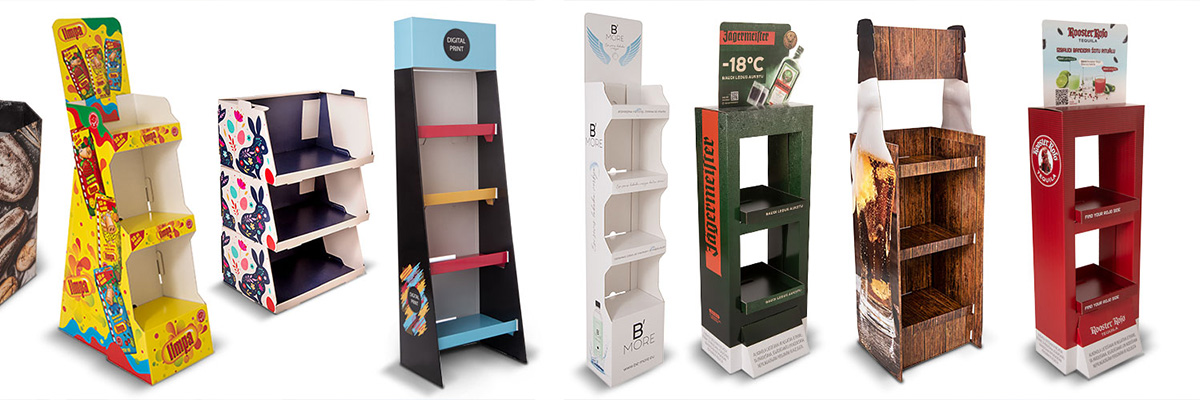
Pre-print flexo works with structural design for shelf-ready packaging. Brands compete for shopper attention. Eye-catching characters and vibrant images on corrugated displays make the difference. Pre-print delivers tighter registration (±1mm). Post-print gives ±2-3mm.
Consumer goods need different standards than industrial uses:
|
Aspect |
Industrial Packaging |
Consumer Goods |
|---|---|---|
|
Durability |
UV-resistant inks for outdoor storage (chemical drums, construction materials) |
Scratch-resistant UV-curable inks for premium shelf appeal (8.42% CAGR) |
|
Graphics Complexity |
Functional printing (barcodes, handling instructions, hazard symbols) |
Bold graphics, metallic effects on natural-fiber substrates |
|
Regulatory Needs |
Serialization codes, tamper-evident varnishes, direct-food-contact approval |
FSC/PEFC green labels, minimum recycled-content thresholds |
Subscription boxes and luxury packaging push flexo further. Micro-flutes need fine plate selection. UV-curable coatings provide scratch resistance at higher line speeds. Brand consistency across SKUs needs 10-color flexo decks paired with CMYK inkjet systems. Premium inside-print for unboxing moments adds production steps.
Future Frontier: The “Plastic-to-Paper” Shift

Beer and soda brands ditch plastic shrink wrap and those six-pack rings fast. They switch to corrugated board carriers (like KeelClip™) instead. This isn’t just a trend. EU laws and US shoppers demand this change. For a print shop, this brings a huge volume chance.
Why Flexo Wins Here
This creates a tough technical problem, and Flexo solves it. These packs must hold heavy, wet cans and survive the fridge. Standard brown board won’t work. You need wet-strength carrier board that handles moisture.
Only Flexo presses run fast enough to match bottling lines. Plus, they apply functional barrier coatings inline. You don’t just print a logo. The press applies a water-resistant varnish that does plastic’s old job. This high-value, high-volume work pushes Flexo past simple logistics.
The “Smart” Bonus
We see these paper carriers turning into data points too. Brands use high-res flexo plates (up to 150 LPI). They print unique QR codes right on the pack to track items or engage buyers. A simple can holder becomes a connected digital asset.
Getting Started: Your 5-Step Flexo Action Plan
You know the pros and cons. Now, execute a flexo project without money loss. Planning stops you from wasting budget on wrong plates or bad inks. Follow this roadmap. We broke the process into manageable phases.
Phase 1: Define Your Production Reality (Week 1)
Get hard numbers before you call a vendor. Annual volume under 10,000 units? Stop here. The ROI stays low. Choose digital printing or litho-lamination instead. Volumes between 10,000 and 50,000 sit in a gray zone. You must run cost comparisons.
Define your quality standard. Retail displays need high precision, around ±1mm registration. Industrial shippers work fine with looser specs, like ±2-3mm. This difference changes equipment budgets by 40%. Pay only for the precision you need.
Create a master spec sheet. Include these details:
-
Exact dimensions: Min/max length, width, and height.
-
Board grade: Use E-flute for ecommerce. Choose sturdy BC-flute for heavy items.
-
Color strategy: 1-color designs cost significantly less than 4-color processes.
-
SKU grouping: Find plate sharing chances. A 300x400mm design runs on the same setup as a 320x380mm variant. You only need minor tweaks.
Phase 2: Build Your Supply Chain (Weeks 2-3)
Find partners, not just vendors. Secure a plate maker, an ink supplier, and a press operator. Ignore the operator if you print in-house. Prices vary 25-35% for identical specs. Get three quotes minimum.
Ask plate makers specific questions. Can they handle rush orders? Do they sell different plate materials like photopolymer or rubber? Match these to your run lengths. Buy a $200 sample plate first. It acts as cheap insurance against a $2,000 wasted run.
Check your ink suppliers. You use water-based inks most often. Verify viscosity ranges. Corrugated board needs 18-25 seconds on a #3 Zahn cup. Get samples in your brand colors. Test them on your actual board. Recycled kraft absorbs ink differently than virgin white liner. Avoid surprises on launch day.
Phase 3: Prototype and Stress Test (Weeks 3-4)
Don’t order 50,000 units immediately. Run a pilot of 100-500 boxes first. Catch design flaws early. Watch for these issues:
-
Score line crowding: Keep text 12.7mm away from folds. This prevents cracking.
-
Opacity: Dark, recycled board absorbs color. You may need a white base layer. This adds cost.
-
Warping: Lightweight boards like E-flute warp at high speeds. This causes registration drift. Test at production speeds, not slow sample speeds.
Review prototypes critically. Check color accuracy. Aim for Delta E < 5. Verify barcode scannability with a real scanner, not a phone app. Test fold integrity.
Phase 4: Production Setup (Week 5)
Schedule the real run during low-demand periods. Operators rush less then. Attend the “make-ready” session. Mistakes show up here.
Watch the setup. Check anilox rollers for cleanliness and spec matching. 360 LPI suits detail work. Verify substrate tension settings to prevent wrinkles. Good operators monitor ink viscosity every 30 minutes. Inspect the first 50-100 impressions closely. Then ramp up speed. A press at 70% speed with low waste beats a maxed-out press with 8% scrap.
Phase 5: Continuous Improvement
Monitor the process constantly. Use in-line inspection. Or, pull edge samples every hour by hand. Track metrics like setup time and registration drift. Target under 5% waste for repeat jobs.
Build a job database. Record effective ink batches. Note machine settings that stopped warp. Compare actual costs to estimates. This data speeds up your next quote. It adds accuracy too. Review results with vendors every quarter. Growing volume helps you negotiate better rates or priority scheduling.
Conclusion
You’ve learned the basics of flexographic printing technique for corrugated packaging. You understand how anilox roller printing transfers exact ink amounts. You can choose between post-print and pre-print workflows for your needs. Plus, you have a framework to decide if flexo printing fits your quality standards, volume needs, and budget.
The real question isn’t whether flexo printing is “good” or “bad.” It’s whether it works for your project. Flexo runs fast for high-volume jobs. It saves money at scale. The packaging industry relies on it. Corrugated box production worldwide uses flexo as its workhorse. Success needs proper flexo press setup. You must know how your material behaves. Set realistic expectations about print clarity.
Ready to move forward? Gather samples from CNN Box. Request test runs with your specific design. Use the troubleshooting checklist from this guide during quality checks. Your journey from beginner to informed buyer starts with that first conversation. You now have the knowledge to ask the right questions and judge the answers well.


