
Staring at a flat piece of corrugated box cardboard and wondering where to start? You’re not alone. Thousands of small business owners, warehouse workers, and even seasoned movers struggle with putting boxes together every day. They waste precious minutes on what should take 30 seconds.
What separates a flimsy box that collapses mid-shipment from a fortress-like container? Knowing the right folding sequence and a few insider techniques.
You might work with standard RSC boxes, sleek mailer boxes, or crash-lock designs. Master the right method for each type. This cuts your packing time by two-thirds. Plus, it reduces product damage during transit.
This guide breaks down how to build every major corrugated box type. You’ll learn the pro shortcuts that professional packers use to work at lightning speed. We’ll show you how to reinforce your boxes to handle 40% more weight. Clear visuals and troubleshooting tips included—all tested in real-world conditions.
What You’ll Need: Tools and Materials for Box Setup

Most corrugated boxes need zero tools. Your hands do all the work. That’s the beauty of flat corrugated packaging—built for speed and ease.
For Standard RSC Boxes:
– Packing tape (2-inch width minimum): Acrylic or hot-melt adhesive types work best. You’ll use 3-4 strips per box on average.
– Tape dispenser: Handheld models with serrated blade cut your taping time in half. The spring-loaded tension keeps tape ready to go.
– Utility knife: Keep one nearby with fresh blades. You’ll need it for trimming extra flaps or opening incoming shipments.
Optional Speed Boosters:
– Box stapler: Heavy-duty staplers secure flaps 40% faster than tape. Pro packers love them for high-volume work.
– Corner protectors: L-shaped cardboard or plastic guards protect weak spots. Must-have for shipping items over 30 pounds.
– Measuring tape: Check that box dimensions match your products. A box that’s 2 inches too large wastes fill material and shipping costs.
Keep your workspace clear. A flat, clean surface helps you work three times faster. Cluttered floors slow you down.
Assembling RSC Boxes (Regular Slotted Container)
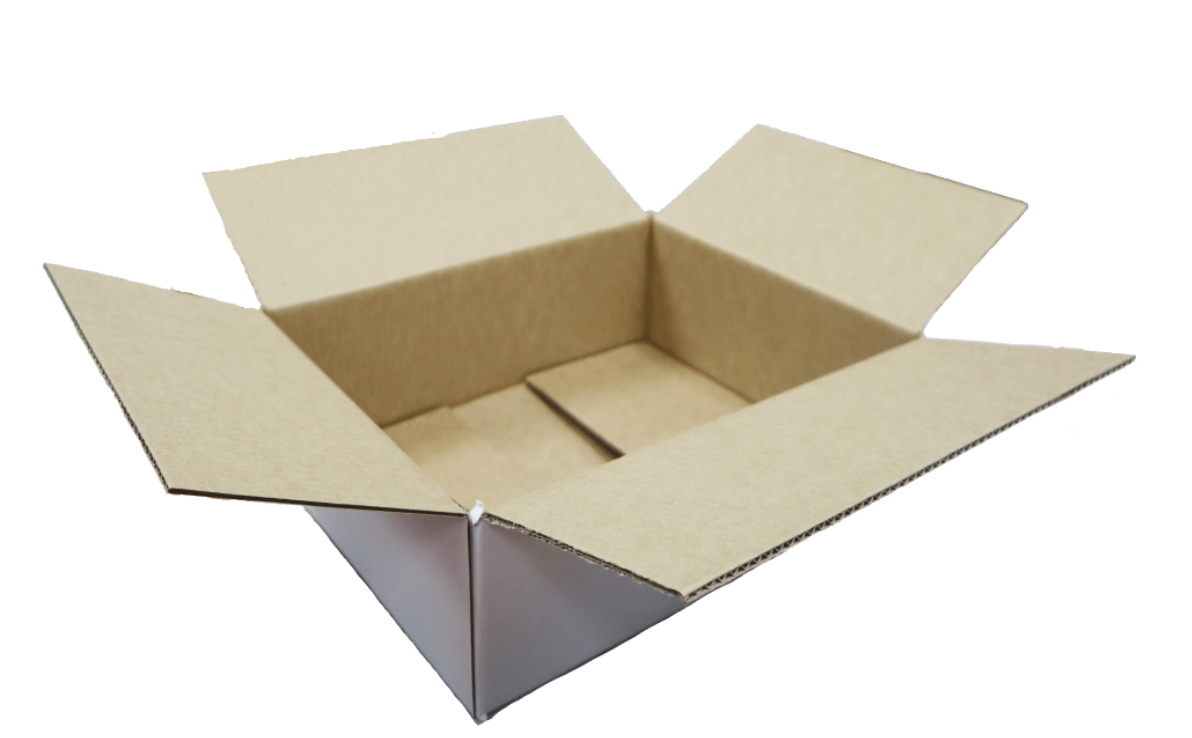
RSC boxes come pre-glued along one edge. The manufacturer seals the vertical seam before shipping. You just fold and tape the bottom and top flaps. Six quick steps get you a ready-to-pack box.
The Basic Steps
Step 1: Pop the Box Open
Grab the flat box by opposite corners. Push the sides out until it forms a tube. The pre-glued seam holds firm. Set the box on a flat surface with one open end facing up.
Step 2: Close the Bottom (Follow This Order)
Fold the two shorter flaps inward first. These end flaps run across the width. They fold at a 90-degree angle along the score line. This closes half the bottom opening.
Now fold the two longer flaps inward. These side flaps span the box length. They meet at the center line. All four flaps now seal the bottom.
Step 3: Tape the Bottom Seam
Run a strip of packing tape down the center where the long flaps meet. Press down hard. This is your main seal. Boxes holding 20+ pounds need two more strips—one along each edge where flaps meet the box body. This H-taping pattern boosts strength by 60%.
Step 4: Load Your Products
Place items inside. Leave at least 1/8 inch of clearance on all sides. This gap stops the box from bulging or splitting at the seams.
Step 5: Close the Top
Repeat the bottom steps. Short flaps inward first. Long flaps second. They align at the center.
Step 6: Seal the Top
Tape the center seam. For fragile items, copy your bottom taping pattern.
Done. One box ready in 30 seconds. No tricks. No guessing. You’ll have it down by your third try.
Assembling Mailer Boxes (Tuck Top Style)

Mailer boxes ship flat and snap together without tape. The tuck-top lid slides into slots along the sidewalls. This self-locking design saves you 15 seconds per shipper. Tape-sealed styles take longer. Plus, your customers can reuse them.
Prep Before You Start
Clear a workspace bigger than your unassembled box sheet. A cluttered table creates bad creases and bent corners. Never stack multiple flat boxes on top of each other while working. The weight damages score lines. This creates weak spots. These spots split during shipping.
The Build Sequence
Step 1: Pre-Crease All Score Lines
Lay the box flat with the printed side down (interior facing up). Find every score line—those thin grooves that mark fold points. Fold each score all the way inward, then release it flat again. This breaks the paper fibers in the right direction.
Pay attention to the sidewalls. Each one has two score lines close together. Fold them one at a time, not as one thick crease. Skip this step and your sidewall gets shorter. The locking tabs won’t line up right.
Never fold past 90 degrees. Don’t press down with your full weight. Gentle pressure does the job. Crushing the flutes destroys the box’s strength.
Step 2: Raise Front and Back Panels
Fold the front and back flaps upward along their score lines. Position the smaller tuck flaps so they sit along the sides. Hold the back flap with one hand. This braces the structure for the next move.
Step 3: Lock the Side Walls
Fold both left and right side flaps over the tuck flaps. Here’s the trick: snap both sides into place at the same time. Push them down together with even pressure. This keeps the box symmetrical and seats the lock tabs correctly.
Check the top edges. They should run flat and level. Slanted or peaked tops mean the tabs didn’t lock. Pop the sides out and try again.
Step 4: Load and Close
Drop your products inside. Close the top lid and slide the locking tabs straight into the sidewall slots. You’ll feel them click into position. No tape. No glue. The box holds firm under normal shipping stress.
Assembling Hand Lock Bottom Boxes
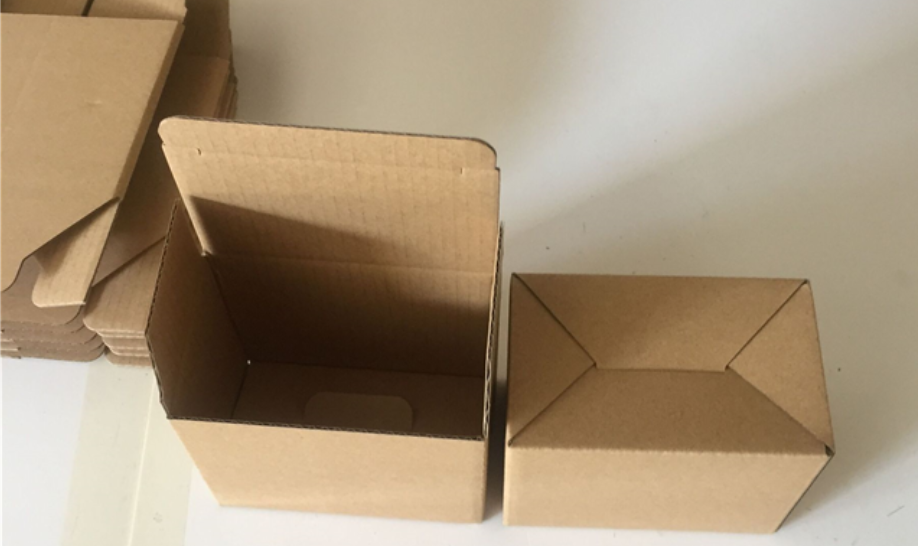
Hand lock bottom boxes ship flat just like RSC styles. The difference shows up at the bottom. Four interlocking flaps fold together and grip each other tight. No tape needed for the base. This design cuts your tape costs by 50% per box. The locked bottom holds 25-30 pounds. You don’t need extra support.
Retail shops love these cartons. Display packaging needs clean bottoms with zero visible tape. The hand lock creates that polished look. Subscription boxes and gift packaging use them too. Presentation matters in these cases.
The Lock-Bottom Build Process
Step 1: Orient the Flat Box
Lay the collapsed box with the bottom flaps facing you. The bottom has four triangular tabs cut into the corners. Two flaps show rectangular cutouts near their edges. Those cutouts are your locking slots.
Step 2: Fold Minor Flaps First
Pop the box into tube shape. Find the two shorter flaps with the rectangular cutouts. Fold these inward at 90 degrees. They sit parallel to each other with a gap between them.
Step 3: Tuck the First Major Flap
Take one longer flap without cutouts. Fold it inward and down. The pointed end slides between the two minor flaps you just folded. Push it all the way through. The flap should lie flat against the box interior.
Step 4: Lock the Second Major Flap
Grab the remaining long flap. Fold it over the top of everything. Its pointed tab slides into those rectangular slots on the minor flaps. You’ll feel resistance as the tab pushes past the slot edges. Keep firm pressure. The tab clicks into place behind the slots.
Step 5: Set the Lock
Press down hard on all four corners where flaps meet. This seats the locking mechanism. Flip the box over and press the bottom center. A locked bottom feels rigid. No flex. No give.
Common Lock-Bottom Mistakes
The second major flap won’t lock? You forced the first flap too far through. Pull it back a bit. This creates space for the locking tab to slide into its slots.
Bottom feels loose? One or both locking tabs missed their slots. Unfold the second major flap and try again. Line up the pointed tab over the slot openings before pushing down.
Triangle corners stick up instead of lying flat? You didn’t pre-crease the score lines. Unfold everything. Crease each score with force. Then rebuild from step one.
Assembling Crash Lock Bottom Boxes
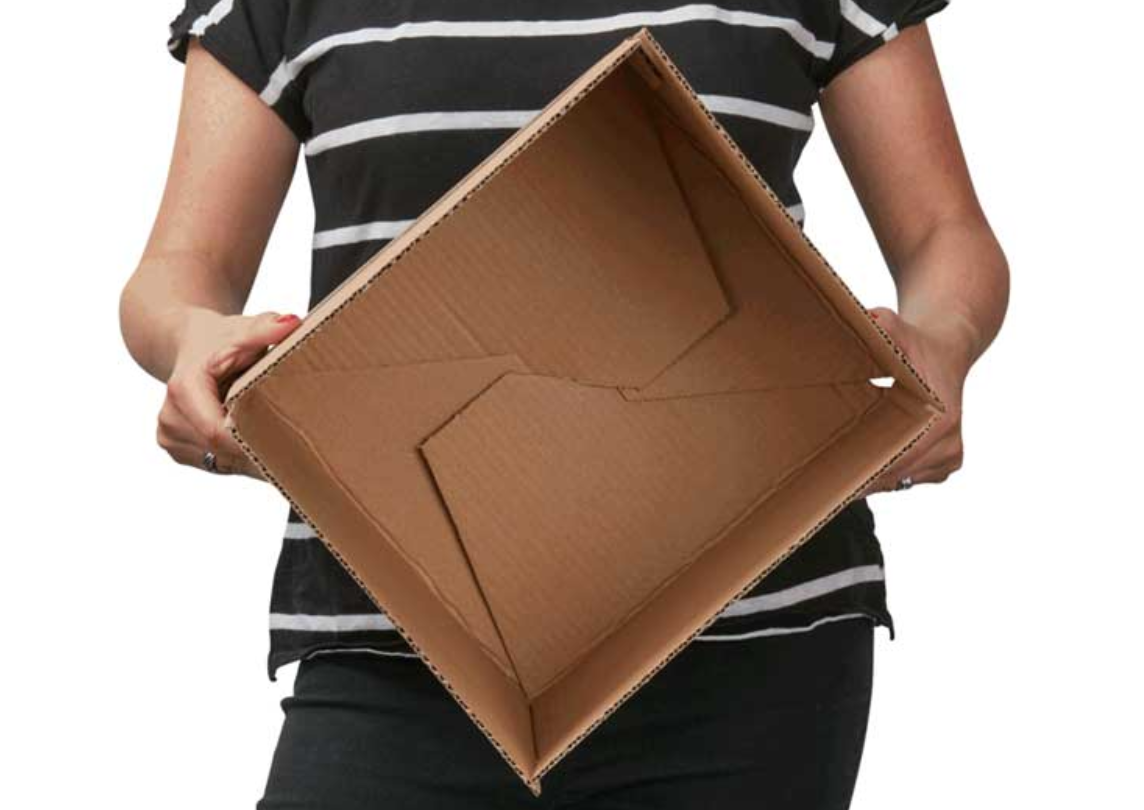
Crash lock bottom boxes hold a speed record no other corrugated style can touch. Two glue points on the bottom panels do all the heavy lifting before the box even reaches your hands. The factory pre-joins every bottom piece. You get a self-locking base that snaps together in under 5 seconds.
E-commerce sellers who pack 200+ orders each day save 10-15 hours per week with crash lock designs. The math is simple: shave 20 seconds off each box and those seconds compound fast. No fumbling with flaps. No taping the bottom. Just pop and load.
These boxes excel at holding heavy products. Candles, glass jars, and bottled goods sit stable on the interlocking base. The dual glue points give you stronger stacking power. Regular fold-bottom styles can’t match this. Stack ten filled boxes high and the bottom one stays square.
The Instant-Lock Build Method
Step 1: Grab the Flat Box
Pick up the collapsed box by its side panels. You’ll notice it feels stiffer than a standard RSC. Those pre-glued points add strength even when flat.
Step 2: Squeeze and Pop
Push both side panels inward with your palms. Press fast. The bottom flaps fold outward as the box opens into tube shape. You’ll hear a soft snap when the glued tabs lock into position.
Some packers prefer pulling the top edges apart instead of squeezing. Either method works. Choose what feels natural for your grip strength.
Step 3: Stand and Verify
Set the box upright on your packing station. Press down on the bottom center. A locked base shows zero flex. The interlocking flaps sit flush against each other with no gaps.
Done. Your box stands ready for loading. Total time: 3-4 seconds per unit once you build muscle memory.
Variable Height Feature
Many crash lock models include built-in crease lines along the sidewalls. Fold at the lower crease for shorter products. Use the upper crease for taller items. This adjustability cuts your SKU count. One box size handles multiple product heights.
Pro Tips: How to Assemble Boxes 3X Faster

Cut out wasted motion. That’s where speed comes from. Pro packers hit 120 boxes per hour. They set up their workspace like a production line. Three core changes get you to that pace.
Set Up Your Station for Zero Movement
Put your tape dispenser within arm’s reach on your dominant side. Stack flat boxes at waist height on your left (or right if left-handed). Place a small trash bin below your work surface for tape scraps and damaged boxes. This triangle layout cuts your reach distance by 70%. Your hands travel less. You pack more.
Pre-cut tape strips waste time. Load a heavy-duty dispenser with 2-inch tape. Use the serrated blade for clean cuts. Spring-loaded models keep tension on the roll. You grab, pull, cut, and stick in one smooth motion. No fumbling with loose ends.
Master the Two-Hand Method
Fold both short flaps at the same time using both hands. Then grab both long flaps at once. Press them together at the center. Single-hand folding doubles your time per corrugated container. Train yourself to work with both hands from day one.
Your first tape strip goes down while you’re still holding the top flap closed. Don’t release the flap, grab tape, then come back. Press the flap. Pull tape with your free hand. Seal in one smooth move.
Batch Your Work in Groups of 10
Build ten boxes at once. Don’t assemble one complete box at a time. Pop open ten tubes. Fold all twenty short flaps. Fold all twenty long flaps. Tape all ten bottom seams. This production-line style builds muscle memory faster. Your hands learn each motion through repetition.
Track your time for each batch of ten. Most beginners start at 8-10 minutes per batch. That drops to 5-6 minutes after 50 boxes. Hit 100 boxes and you’ll clear ten boxes in under 4 minutes. Consistency beats speed at first. Good work prevents expensive re-work.
Strengthening Techniques: Making Boxes 40% More Durable

Standard corrugated boxes work fine for everyday shipping. Heavy products need more protection. Rough handling and long trips can damage them. A few simple methods boost box strength by 30-40%. Your products stay safe. Damage claims drop.
Reinforce High-Stress Points with Hot Glue
Hot glue turns weak joints into strong zones. Put a thick bead along each bottom corner. Focus on spots where flaps meet the sidewalls. Press the pieces together for 5 seconds. Let the glue set. Run the glue gun tip over all exposed edges for full coverage.
This method dries in 60-90 seconds. White glue and wood glue take 20-30 minutes. Hot glue gives you instant strength. Boxes fixed this way handle an extra 8-10 pounds before joints separate.
One warning: skip hot glue if you plan to paint or print on the box. The glue bleeds through paper coatings. It creates bumpy spots. The finish won’t look good.
Upgrade Your Sealing Method
Cheap packing tape breaks under stress. Boxes over 25 pounds need commercial-grade tape with 1.9 mil thickness or higher. Acrylic types grip better than rubber-based ones in cold warehouses.
The H-taping pattern adds real strength. Run one strip down the center seam. Add two more strips along each edge. Place them where bottom flaps meet the box body. This creates an H shape. The triple-layer seal spreads weight across three bond lines instead of one.
Heavy-duty staplers work faster than tape for big operations. Pro box staplers drive 1-inch staples through triple-wall cardboard in one squeeze. Each staple holds 15-18 pounds of force. Four staples per seam replace three tape strips.
Finish Cut Edges to Prevent Tears
Rough edges from knife cuts create weak spots. These frayed fibers catch on conveyor belts and forklift forks. Small tears turn into major splits during shipping.
Sand all cut edges with 80-grit sandpaper. Make 3-4 quick passes along each edge. This removes loose fibers. It softens sharp corners. The smooth finish resists catching and tearing. Your boxes make it through the trip intact.
Total time per box: 15-20 seconds of sanding. Check your damage rate reports. You’ll see the payoff.
Troubleshooting Common Box Problems

Boxes fail for three main reasons. Bottom flaps won’t stay closed. Corners split as you load products. Tabs refuse to lock into slots. Each problem has a fix that takes under 60 seconds.
Bottom Flaps Pop Open After Taping
Your tape isn’t sticking to the cardboard surface. Dust, moisture, or oil from your hands creates a barrier between adhesive and paper. Wipe all flap surfaces with a dry cloth before taping. The tape bonds 3x stronger on clean cardboard.
Cold warehouses kill tape grip. Acrylic tape loses 40% of its holding power below 50°F. Switch to hot-melt adhesive tape for cold storage areas. Store your tape rolls at room temperature. Cold tape won’t stick even on warm boxes.
Check your tape width. Anything under 2 inches lacks the surface contact needed for heavy duty boxes. Narrow tape peels at the edges first. Use 2.5-inch or 3-inch tape for loads over 20 pounds.
Corners Split or Tear During Setup
Forcing flaps past 90 degrees damages the paper fibers at score lines. Fold to the crease line and stop. Don’t press down with your full body weight. Too much pressure breaks the corrugated structure.
Old boxes sitting in humid storage lose 30% of their strength. Moisture softens the adhesive between paper layers. The flutes collapse easier. Touch the sidewalls. Soft or spongy cardboard means water damage. Toss these boxes. They’ll fail during shipping.
Rough handling creates micro-tears you can’t see. These invisible cracks spread as you fold the flaps. Slide boxes—don’t drop them. Store flat boxes in stacks under 4 feet tall. Heavy stacks crush the bottom units.
Lock Tabs Won’t Snap Into Slots
Misaligned score lines cause this 80% of the time. The factory cut the slots in the wrong position. Grab the sidewall and flex it outward a bit. This widens the slot opening by 2-3mm. The tab slides in with light pressure.
Bent or crushed tabs can’t lock right. Flatten damaged tabs with your thumb before inserting them. Press against a hard surface to reshape the cardboard. Badly damaged tabs need reinforcement with a small piece of tape on the underside.
Box Stays Lopsided After Setup
You didn’t fold opposite flaps at the same time. Folding one side first pulls the box out of square. The structure sets in that twisted position. Unfold it all. Start over and fold both short flaps together using both hands. Then fold both long flaps at once. Equal pressure on opposite sides keeps the box straight.
Conclusion
Let’s be real: putting corrugated boxes together isn’t the fun part of business. Yet, we’ve seen it is vital. You now have the skills to handle it all. From standard RSCs to crash-lock designs, you can do this work easily.
Speed counts. Saving time on your packing routine is a win. But confidence counts more. Fold and seal a box right. Then you know it handles the rough trip. Stop hoping it survives. Make sure it does.
So, use these methods in your warehouse. Bring them to the packing table. Teach your team the right moves. That box is the first thing your customer touches. It speaks for your brand. Let it show that quality matters to you.


