

Looking for a custom label manufacturer that meets all your requirements—one with expertise, guaranteed quality, custom services, and reliability? You’re not alone. Choosing the right partner isn’t just about printing a logo on paper. It’s about finding a team that understands your industry’s unique demands, delivers labels that perform flawlessly in real-world conditions, and aligns with your brand objectives.
In this guide, we’ll break down 7 critical factors for effectively evaluating manufacturers: industry experience, material durability, production capacity, printing technology, pricing, and customer service. Whether you’re in healthcare, food, electronics, or consumer goods, these insights will help you avoid costly mistakes, optimize your supply chain, and find a partner who grows with you. Let’s dive in.
Factor 1: Experience and Industry Expertise
I recommend choosing a custom label manufacturer based on their experience and industry expertise. These factors build quality, reliability, and compliance.
Years in Business and Track Record
I suggest prioritizing manufacturers with a proven history. For example, CNN Box has served the life sciences sector for over 20 years. Look for companies with at least 5 years of continuous operation in your sector. Long operation shows resilience and improved processes.
Ask for statistics. Request their on-time delivery rate (look for 97%+ rates) or low claims frequency. These numbers show operational excellence and reliability.
Specialized Industry Knowledge
Pick manufacturers who specialize in your product area. This could be medical, pharmaceutical, food, or electronics.
Sector expertise means they know unique requirements. Circuit board label suppliers must offer solutions that resist high temperatures and chemical exposure. Food packaging may need custom adhesives or tamper-evident security features.
For medical and pharmaceutical labels, I recommend finding experience with strict regulatory environments. They should deliver labels that meet all compliance needs.
Regulatory Compliance and Certifications
Check that manufacturers hold certifications like ISO 9001:2015. About 70% of pharmaceutical label makers have this certification. In consumer labeling, 50% have it.
Confirm they get regular third-party quality audits. FDA-regulated label suppliers go through 1-3 audits per year. Each audit lasts about two days.
Make sure the company meets industry-specific standards. These include FDA, GMP, UL, REACH, and RoHS.
Key Questions to Ask
- How long have you produced custom labels for my product type?
- Can you provide up-to-date certifications and audit records?
- Have you solved specific compliance or durability challenges in my industry?
Based on my experience, I recommend focusing on these criteria. Seek clear evidence. This will help you select a custom label manufacturer with real expertise and a strong industry track record.
Factor 2: Quality of Materials and Printing
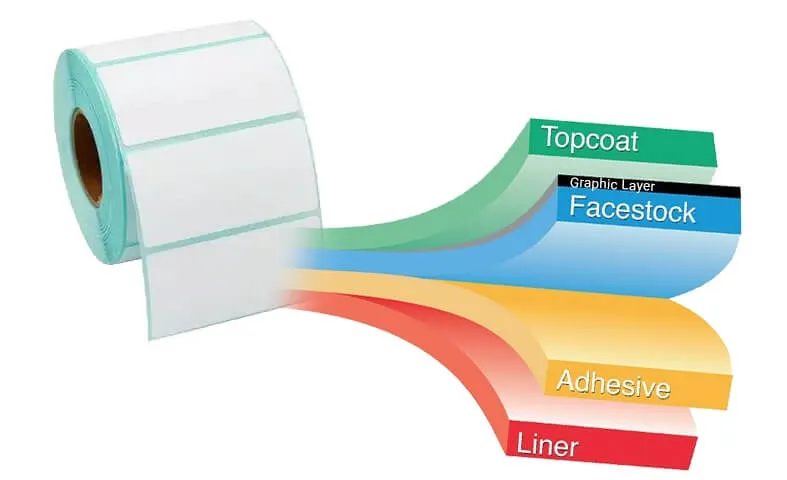
A custom label’s performance relies on two things: the materials the manufacturer picks and how well they control print quality. Both must fit your exact needs. This is especially true for tough applications.
Types of Label Materials and Their Properties
I suggest you choose a manufacturer with many label materials that fit your product’s use. Here are some options:
Clear BOPP: This material is transparent. It resists water, oil, scratching, and temperature changes very well. I recommend it for food and cosmetic packaging.
Metallic Foil: This gives a bright finish and sticks permanently. It resists heat and chemicals better than most materials. Use it for luxury goods and products in harsh environments.
Kraft Paper: This is 100% recycled and eco-friendly. It has a rustic look. Artisan and organic brands prefer it.
Standard Paper: You can get gloss and semi-gloss options. It resists water and oil. Use it for general consumer packaging.
Print Durability and Quality Control
Good manufacturers use these methods:
Smudge-proof inks and high-resolution printers make graphics and text crisp.
Routine in-line quality checks: They inspect at each step—printing, lamination, cutting. They do final reviews with special lighting or barcode scanners.
Quality certifications: Look for ISO 9001:2015 or similar. This shows they control quality systematically.
Fact: Medical labels must survive sterilization (autoclave, gamma radiation). They must also resist harsh chemicals like xylene and isopropyl alcohol.
Sampling, Testing, and Real-World Validation
Most experienced manufacturers give you free samples or test prints. I recommend you test label samples in conditions that match real use: heat, cold, chemical exposure, and abrasion. For example, custom food packaging labels should resist freezers and moisture. Industrial labels must handle oil and sunlight.
Summary Table: Essential Label Materials
| Material Type | Key Features | Main Applications |
|---|---|---|
| Kraft Paper | Eco/rustic, recycled, resists moisture | Artisan & sustainable brands |
| Metallic Foil | Resists heat/chemicals, vibrant | Luxury goods, electronics |
| Clear BOPP | Resists water/oil/temp/scratches | Cosmetics, bottles, outdoor goods |
| Standard Paper | Glossy, resists water/oil | General packaging |
I always insist on sample testing based on your application. Request proof of certifications. This ensures your label’s material and print quality match your product needs and meet regulatory rules.
Factor 3: Customization and Design Capabilities
I recommend comparing custom label makers based on their customization and design skills. This ensures your labels stand out and work well.
Custom Shapes, Sizes, and Specialty Finishes
Find makers that offer many custom label shapes and sizes. I like circles, ovals, rectangles, die-cut, layered, and peel-back designs. Material choice matters. Options should include paper, plastic, metallic, clear, and textured types. These help your brand create unique looks. They adapt to any package style.
Over 70% of top CPG brands invest in special finishes and unique shapes. This boosts shelf impact. It strengthens brand identity. I suggest looking for matte, gloss, soft-touch coatings, metallic foiling, embossing, spot varnish, and tactile elements. These improve visual appeal. They add tactile interest. They raise perceived quality.
Design Support and High-Resolution Printing
Your supplier must handle detailed artwork and visuals. High-resolution digital printing is key. 300 DPI or higher is standard for clarity. Makers should provide pre-press technical checks. This includes support for various file formats. It includes precise CMYK or Pantone color management. Clear bleed specs matter too (1/16th inch for full-bleed designs).
Leading makers offer in-house design help. Or they work well with your external design team. They guide you in choosing the right materials and finishes. They support you through the design, prototyping, and printing stages.
Prototyping, Proofing, and Lead Times
Efficient proofing and prototyping matter. Lead times for proofing and full production range from 3–10 business days with digital print specialists. Digital proofs are standard. For detailed finishes or shapes, physical press proofs or prototypes should be available. These often cost extra. Most makers customize the proofing process. This catches errors. It reduces risk before full production.
Key Questions to Ask Suppliers
- Can you handle special die-cuts, clear or textured materials, and advanced embellishments?
- Do you offer in-house design resources and technical guidance for artwork prep?
- What is your experience with complex or regulated label types? (Think pharmaceuticals, food safety, certifiable marks)
Based on my experience, I suggest selecting a maker proven in delivering custom design and broad customization. Look for this from initial concept through final production. This ensures maximum label impact and compliance.
Factor 4: Production Capacity and Lead Times
I recommend choosing a custom label manufacturer with the right production capacity and flexible lead times. This helps you avoid bottlenecks, missed launches, or gaps in your label stock. These factors matter most for brands with seasonal demand, fast product cycles, or rapid growth.
Minimum and Maximum Order Quantities (MOQ and Capacity)
Leading label manufacturers set MOQs between 1,000 and 10,000 units. This depends on printing technology and materials. Maximum production capacity can exceed millions of labels per month for large converters. Avery Dennison, CCL Industries, and CNN Box can handle runs above 5 million labels per month. They use both digital and flexographic presses. Ask for detailed production range stats. Volume flexibility of ±20–30% on orders is common among top-tier suppliers.
Typical and Rush Lead Times
Standard lead times: Most manufacturers promise 5–10 business days for regular orders.
Complex or custom orders: Expect turnarounds of 10–20 days.
Rush services: Urgent projects can be delivered in 3–5 days for a premium fee. Digital printing makes this possible.
Digital printing allows for fast turnaround. Small batch runs take as little as 2–3 days. Flexo or offset requires longer prep times.
Scalable Production and Vendor-Managed Inventory (VMI)
Many manufacturers offer vendor-managed inventory (VMI) programs. They hold stock for clients and provide just-in-time delivery. This reduces your warehousing costs. It also prevents out-of-stocks. Brands that face seasonal spikes (such as beverages or food products) should find suppliers that can scale up capacity by 2–3x during peak times. Speed and quality should not suffer.
Technology-Driven Solutions for Capacity
Domino Printing Sciences: Delivers high-speed digital systems. These can print up to 44,000 bottles per hour. This is ideal for high-volume beverage labels.
HP Indigo: Offers digital presses that support short runs and rapid design changeovers. Flexible batch sizes work well for promotional campaigns or frequent rebrands.
Hybrid systems (flexo + inkjet): Enable efficient switching between large jobs and variable-data work. This maximizes plant productivity.
Key Questions to Ask Suppliers
- What are your minimum and maximum order sizes?
- What is your typical lead time for both standard and complex custom orders?
- How do you handle seasonal demand spikes or urgent promotional runs?
- Do you provide vendor-managed inventory or just-in-time delivery?
- How do you manage production delays or capacity bottlenecks?
Based on my experience, a strong custom label manufacturer should offer scalable capacity, fast lead times, and the transparency you need. This ensures you meet every launch and peak season with confidence.
Factor 5: Technology and Printing Capabilities
Modern label manufacturing needs advanced printing technologies. These technologies deliver high-quality, customizable, and cost-effective labels. The right technology affects print durability and design flexibility. It also impacts speed and price. I suggest you examine the manufacturer’s investment and expertise in this area. Check what equipment they use and how often they update it.
Core Printing Methods: Digital, Flexographic, and Hybrid Systems
Digital Printing: I recommend this for short runs (under 10,000 units). It works well for frequent artwork changes and multiple SKUs. There are no plate costs. Turnaround time is often 30–50% faster than flexo. Digital excels at variable data printing. It supports 100% label personalization in every run.
Flexographic Printing: This is most efficient for large volumes (above 10,000 units). It’s also cost-effective at scale. Flexo produces consistent colors and finishes. It uses high-speed plate-based production. Flexo allows for strong specialty finishes. It delivers the lowest unit costs at scale.
Hybrid Printing: This combines digital and flexo advantages. It enables spot varnishes, metallic inks, gradients, and security features (serialization, QR codes). All can be applied at the same time. It supports rapid job switching and inline finishing.
Leading-Edge Equipment Examples
Bobst Master M5 Flexo Press: Print quality up to 120 lpi. Automated workflows. Inline finishing. Multi-web for shrink sleeves and pressure-sensitive labels.
Gallus Labelmaster Advanced: Flexo and digital integration. Inline embellishments. Multicolor and screen printing. Ideal for high-volume and high-security labeling.
Nilpeter FA-Line: Modular design. Automated clean-up. Closed-loop color control. Sleeve-based units for pharma and cosmetics. Minimizes waste and human error.
Technological Features That Matter
Variable Data Printing (VDP): Supports serial numbers, barcodes, QR codes. Key for traceability, regulatory compliance, and personalized marketing.
Serialization: Guarantees unique identification on every label. Essential for pharmaceuticals, electronics, and luxury goods.
Specialty Finishes: Spot varnishes, metallics, textured or embossed effects. All applied inline for efficiency and branding impact.
Automation: Quick job presetting. Inline finishing modules. Automated cleanup. These improve run consistency and minimize downtime.
Sustainability: Waste reduction and advanced controls help meet corporate eco goals. Nilpeter’s intelligent waste systems are a good example.
Key Questions for Your Supplier
- Which printing technologies are in use (digital, flexo, hybrid)?
- Are high-speed variable data printing and serialization supported?
- Can specialty finishes (metallic, spot varnish, gradients, textures) be done inline? Or do they require a secondary process?
- How do you ensure fast job changeovers and minimize production waste?
I recommend: Target manufacturers who invest in advanced equipment. Look for those who update their systems often. Their range of printing, finishing, and data capabilities will future-proof your labels. You’ll be ready for compliance, security, and brand differentiation.
Factor 6: Transparency in Pricing and Terms
Clear pricing and contract terms help you build trust with your custom label manufacturer. They also help you manage costs better. Without this clarity, you face unexpected charges. Budget overruns become a real risk. Here’s what I recommend you look for:
Breakdown of Label Costs and Pricing Structure
Always request a detailed, upfront quote. The quote should itemize all costs. This includes custom materials, printing, finishing, and setup. Base custom label costs change based on your choices. For example, standard labels might be $0.50 each using basic materials. Premium materials or finishes can push the price up to $1 each. Think about how materials, inks, and embellishments affect price. Specialty inks, metallic, or fluorescent finishes increase your costs by 10–30%.
Setup Fees, Minimum Order Quantities (MOQs), and Hidden Costs
Ask about all setup fees upfront. These often range from $50 to $300 per run. The cost depends on design complexity and tooling.
Ask about minimum order quantities. Most manufacturers set MOQs at 500–1,000 units. If you need fewer, expect possible surcharges.
Watch for hidden fees. These include charges for digital proofs, die-cut tooling (often $25–$50), rush orders, or variable data printing. Make sure your quote includes these.
Additional Cost Factors
Shipping and packaging can change your final price. This is true if you need fast shipping or custom packaging solutions. Some suppliers reveal certain fees after you ask. Always probe for extra charges. These relate to rush production or special compliance needs.
Key Questions for Suppliers
- Can you give me a complete pricing breakdown for all materials, print options, and finishing?
- Are there setup charges, MOQs, or tooling/design fees? How much for each?
- Will you provide a written quote showing all charges, taxes, and shipping before production begins?
- Could my price-per-label rise after your quote? How would you inform me if that happens?
I recommend you always insist on a written, itemized quote. Work with custom label suppliers who explain every charge. Good suppliers help you understand costs. This way, you avoid surprises. You get the best possible value. Industry leaders stress that open dialogue helps. Share your needs with them. Listen to their advice. This can help you reduce waste. It also cuts unnecessary expense.
Factor 7: Customer Service and Communication

Good customer service and clear communication matter a lot. I recommend you check this first before choosing a custom label manufacturer. Industry data shows over 60% of business clients switch label suppliers due to slow or unclear communication. Fast responses, timely updates, and professional support rank in the top three drivers of customer satisfaction and loyalty.
Key Aspects of Customer Service in Custom Label Manufacturing
Multiple Support Channels: Top manufacturers give you many ways to reach them. You can use live chat, phone, and email. Some offer 24/7 support or promise responses within 2 hours.
Dedicated Account Managers: Leading suppliers assign one person to handle your account. This solves issues 32% faster on average. It also cuts project delays. 78% of small businesses report smoother projects when working with a designated manager.
Automated and Transparent Communication: Good suppliers send you automatic updates. You get alerts at key stages: order confirmation, production start, shipment, and any changes. You learn about problems or delays right away.
Efficient Issue Resolution: I suggest you ask suppliers about their process. Find out how fast they solve delivery or quality problems. The best providers fix issues in 1–2 business days. Ask how they handle urgent requests.
Clear Return and Correction Policy: Trusted manufacturers make returns simple. They fix incorrect or defective labels fast. Most provide replacements or refunds within 7–14 days.
What to Ask When Assessing Suppliers
- What support channels do you offer (live chat, phone, email)?
- Will I get a dedicated account manager for my project?
- How fast do you respond to questions and issues?
- Can you share recent customer service examples?
- What is your process for urgent changes or rush custom label orders?
- How will you keep me informed about my order status and changes?
- How do you fix defective or wrong orders?
Evaluation Criteria: Customer Service Checklist
Response Time: Top suppliers answer within 1 hour for urgent requests. The industry average is under 4 hours.
Reliability: Look for positive reviews and references about service quality and fast, clear communication.
Proactivity: Good suppliers tell you about delays or issues before you find out on your own.
Follow-Through: Suppliers keep logs of client concerns. Some give you dashboards or reports to track issue resolution.
Return Handling: Standard policies include replacements or refunds processed within 7–14 days.
Based on my experience, a custom label manufacturer with responsive, reliable customer support and clear communication is essential. It cuts risk. It speeds up issue resolution. It builds trust for long-term partnerships.
Choosing the right custom adhesive label manufacturer is key for your business. The 7 factors here help you pick a reliable partner easily. At CNNBox, we offer industry expertise, top-quality materials, flexible customization and clear service. Whether you’re launching a new product or optimizing your supply chain, a good label partner turns a small detail into an advantage. Ready for high-performance, standout labels that match your brand? Let’s start your journey today.


