

You’ve seen the finished CNN Box on the shelf—crisp logos, aligned folds, colors that pop just as your brand team intended. But how does a Cardboard box achieve that level of consistency, batch after batch, order after order?
Most packaging factories treat quality like a checkbox. We treat it like a religion. Our <0.8% defect rate didn’t happen by accident. It’s the result of precise control across four key stages.
First, Printing locks in your color whether CMYK or Pantone within 1.5 $\Delta E$. Second, die-cutting stays accurate to $\pm 0.1$ mm. Third, finishing adds tactile luxury. Fourth, our Lean QC system catches flaws before they become your problem.
Walk our production floor and see why your CNN boxes arrive camera-ready, every single time. No fluff. No theory. Just the machinery, the metrics, and the careful details that separate premium packaging from basic cardboard.
Real-Time Detection That Catches What Human Eyes Miss
Most factories still depend on human eyes and hope. We use advanced Automated Optical Inspection (AOI) systems. They assist our QC team in deciding whether your box passes or fails in milliseconds.
The difference shows up in numbers you can bank on. Our production floor runs automated checks at every critical checkpoint. Print registration, die-cut precision, glue adhesion, surface finish—the system spots tiny defects that tired human eyes miss. Grain irregularities. Color shifts as small as 0.5 $\Delta E$. Structural weak spots that would fail during shipping.
Predictive Maintenance stops surprise failures. We don’t just inspect the boxes; we monitor the machines making them. Worn cutting plates? Misaligned print heads? The system flags these issues before they create a single bad unit. Result? 50% reduction in unplanned downtime. Your order doesn’t get delayed because a die-cutter failed mid-run.
Section 1: The Print — Why Your Brand Color Never Drifts
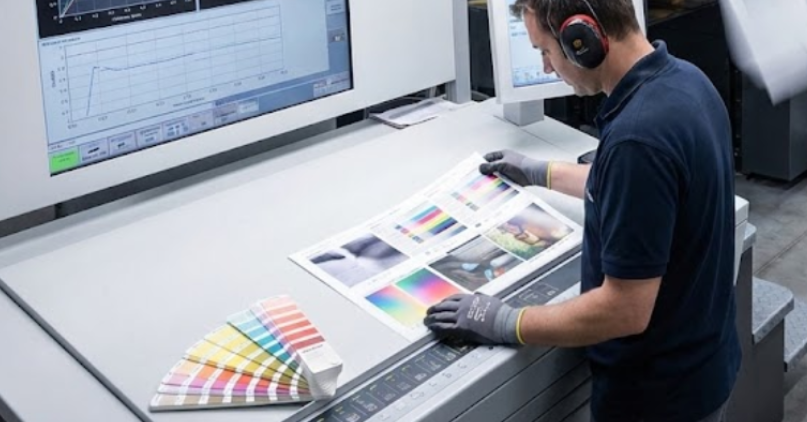
Brand recognition jumps 80% with consistent colors. That’s the difference between a customer grabbing your CNN Box or walking past it. Most packaging factories guess at color matching. They rely on “visual checks” and hope the ink density stays stable.
We don’t guess. We use the Heidelberg Speedmaster 6-1050 Six-Color Offset Press. Whether running complex CMYK imagery or strict Pantone spot colors, your brand stays within 1.5 $\Delta E$ tolerance from box one to box ten thousand. Here’s how we stop color drift before it reaches your brand.
CMYK & Pantone: Mastering Both Spectrums
Your design might need the rich, photographic detail of CMYK or the pinpoint accuracy of a Pantone solid. We don’t force you into one lane. We master both.
- For Complex Imagery (CMYK): When your box features product photos or gradients, we utilize the Heidelberg’s precise 4-color process blending. Our automated density scanning ensures that the mix of Cyan, Magenta, Yellow, and Black remains balanced, preventing “muddy” images.
- For Brand Precision (Pantone): For your signature logo—that specific “Royal Blue” or “Sunset Orange”—we recommend Pantone matching System (PMS) pre-mixed inks. This delivers the exact hue your brand guide demands, with zero interpretation error.
Calibration Discipline: Why We Check Equipment Daily
Color accuracy needs constant care. Press rollers wear down. Inking systems shift. These small changes add up to visible color shifts.
We run daily checks on critical equipment. Not because rules require it. Because your brand color can’t handle 30 days of slow drift. We measure output against digital standards before production starts. Readings fall outside $\Delta E$ 1.5 tolerance? The press stops until we fix it.
Most factories check once a month. Then they wonder why batch five looks different from batch one. We catch the drift before it becomes a problem.
Section 2: The Cut — Precision to ±0.1mm
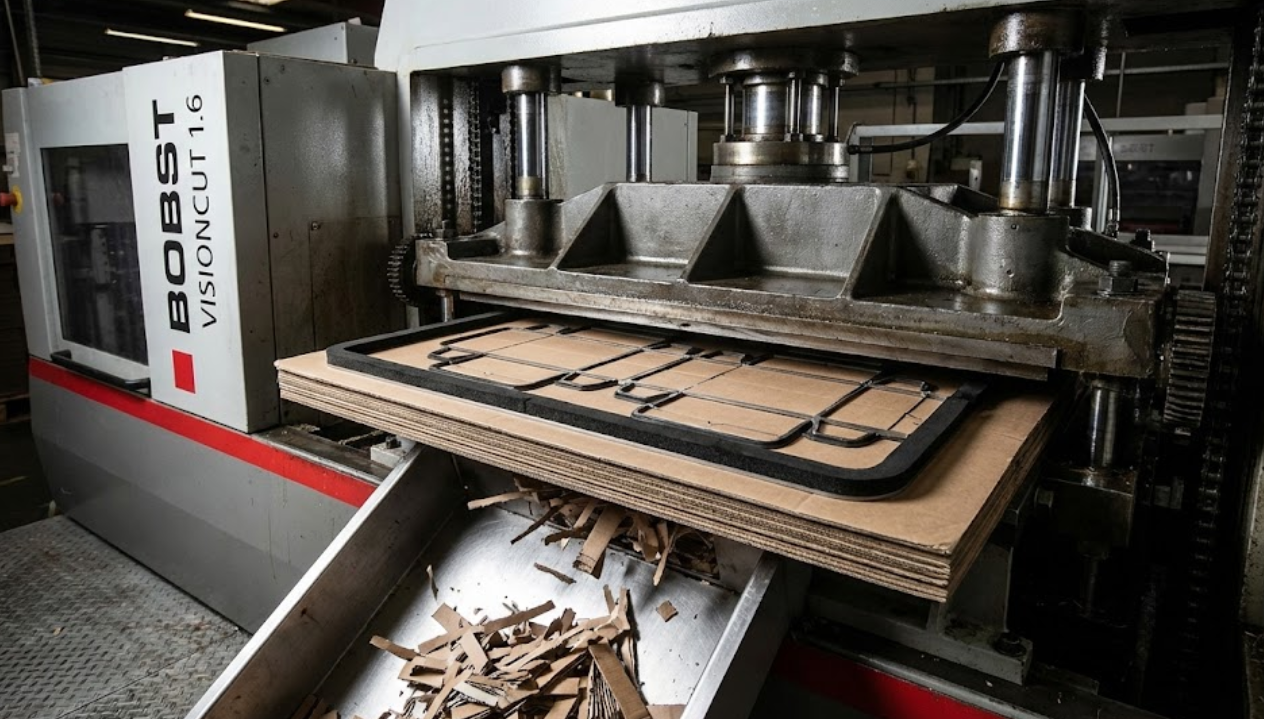
Die-cutting separates premium packaging from garbage that falls apart in transit. A tenth of a millimeter—that’s the tolerance your CNN Box needs. It folds clean. It stacks right. It survives the beating of logistics chains. Miss that mark? You get misaligned flaps, weak corners, and boxes that collapse under light weight.
We hold $\pm 0.1$ mm cutting accuracy across every production run. That’s significantly more precise than old rough-cutting methods. The difference shows. Your boxes arrive with edges that line up right. Folds crease where they should.
The Machinery: Swiss Engineering, Not Guesswork
We don’t rely on repurposed digital cutters for mass production. We use the BOBST VISIONCUT 1.6 Fully Automatic Die-Cutting Machine.
While digital cutters (like JWEI) are great for prototyping samples, they can’t match the consistency of a dedicated industrial die-cutter for volume runs. The BOBST VISIONCUT ensures that every sheet is clamped, cut, and stripped with identical pressure.
Why Precision Matters for Your Brand
Most factories talk about speed. We focus on stability. The BOBST system ensures that the 10,000th box is cut exactly the same as the 1st box. No “drift” as the machine heats up. No ragged edges from dull blades.
Our automated waste stripping removes the excess paper cleanly. This means when your fulfillment team opens the carton, they grab a ready-to-assemble box, not a piece of cardboard covered in paper scraps. Faster assembly for you means lower labor costs.
Section 3: The Finish — Luxury You Can Feel
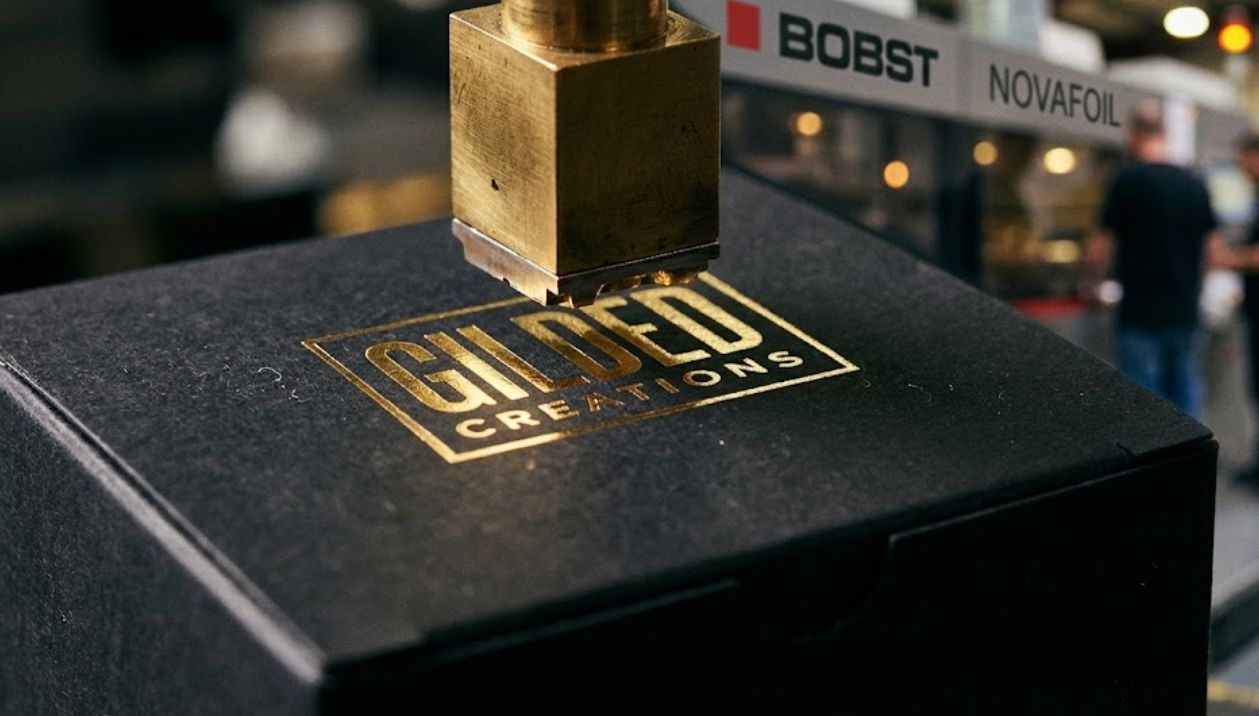
Touch separates premium from passable. Your CNN Box doesn’t just hold product—it introduces your brand before anyone reads a word. The texture under fingertips matters.
We bring the same focus to packaging as luxury watchmakers. Not because cardboard deserves watch-level attention, but because your customer’s first physical touch with your brand happens through a box.
Lamination & Coatings: Protection That Enhances
Matte lamination stops fingerprints and scuffs. gloss lamination makes colors punch harder.
We use the BOBST NOVAFOIL 106H for Foil stamping and finishing. With a yield rate of up to 99.8%, it ensures that every metallic detail is crisp, unblemished, and perfectly aligned. No peeling foil. No misaligned Spot UV.
The finish isn’t just decoration. It’s the final defense between your brand and the chaos of logistics. Choose right, and your box survives the journey looking showroom-ready.
Gluing: Speed Meets Strength
A box is only as good as its glue bond. We use the Bobst Expertfold 110 A2 Folder-Gluer. It runs at 800 pieces per minute—that’s 5x faster than manual gluing. But speed isn’t the only benefit. The machine applies the exact amount of adhesive every time. No messy overflow (which ruins the look) and no weak spots (which cause boxes to pop open).
Section 4: The Control — Our “Lean QC” System
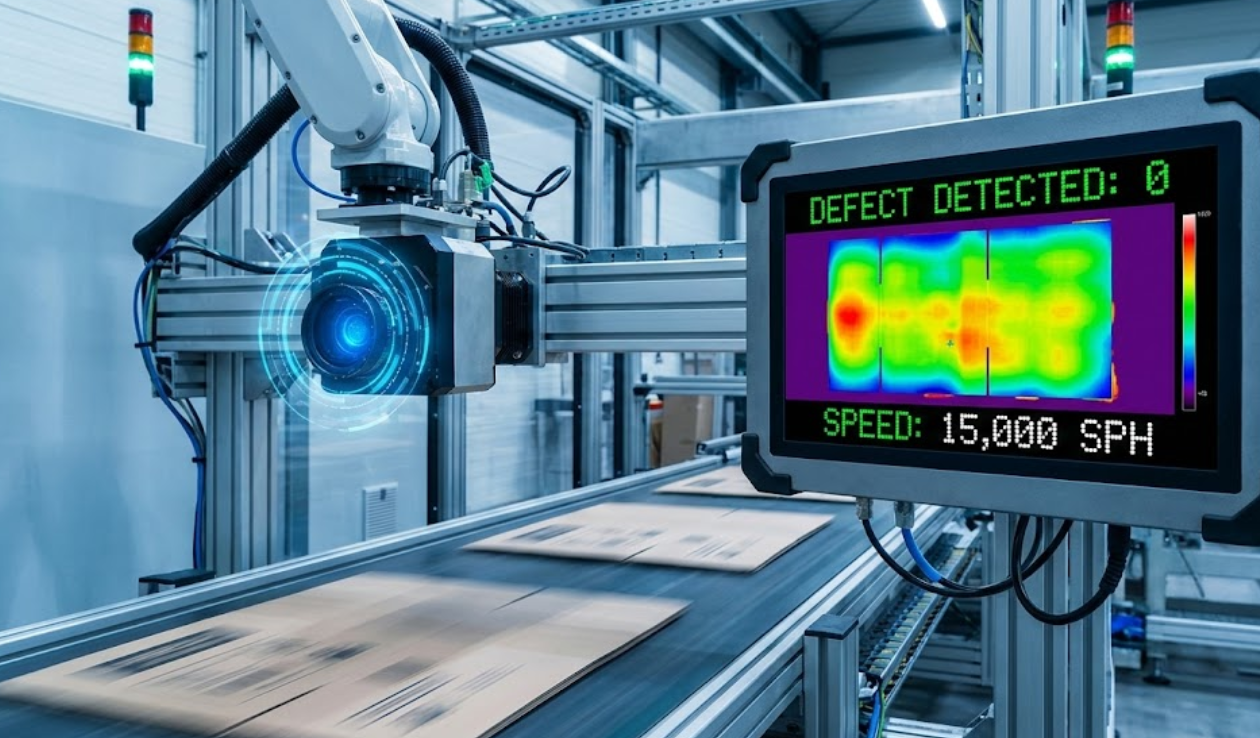
Most packaging plants check quality after problems show up. We check before production starts. Reactive inspection waits. Predictive control acts first.
DMAIC Integration: Define, Measure, Analyze, Improve, Control
Lean Six Sigma gave us the framework. We built the execution system around it. DMAIC runs here as an everyday operation.
- Define: We identify critical quality parameters specific to your order (e.g., Color tolerance < 1.5 $\Delta E$).
- Measure: Sensors on printing presses capture color density.
- Control: Automated alerts notify supervisors about parameter drift.
The Result: <0.8% Defect Rate
Industry-standard defect rates often sit around 3-5%. We run consistently below 0.8%.
This means fewer rejections, fewer returns, and fewer emergency replacements that disrupt your launch schedules. We treat cardboard with the same discipline that tech manufacturers use for electronics.
Your boxes achieve consistency because we measure, predict, and correct before problems show up. Quality control reacts. Quality assurance prevents.
Conclusion
Quality isn’t an accident. It’s built into every fold.
Walk through any packaging factory and you’ll see machines running. Walk through ours, and you’ll see a different picture. Sub-millimeter precision guides every cut. Our color science stays consistent across 50,000-unit runs. The QC protocol catches defects most suppliers miss.
That <0.8% defect rate? It’s not luck. Heidelberg presses get calibrated each week. BOBST cutters ensure structural integrity. The finish work transforms corrugated board into something your customers want to keep.
Your CNN Box should do more than protect product. It represents your brand. Think of it like your website, your storefront, your promise to customers.
Want to see the difference? Request a factory sample with your exact specs. We’ll print it, cut it, finish it, and ship it to you. No sales pitch. Just proof.


