
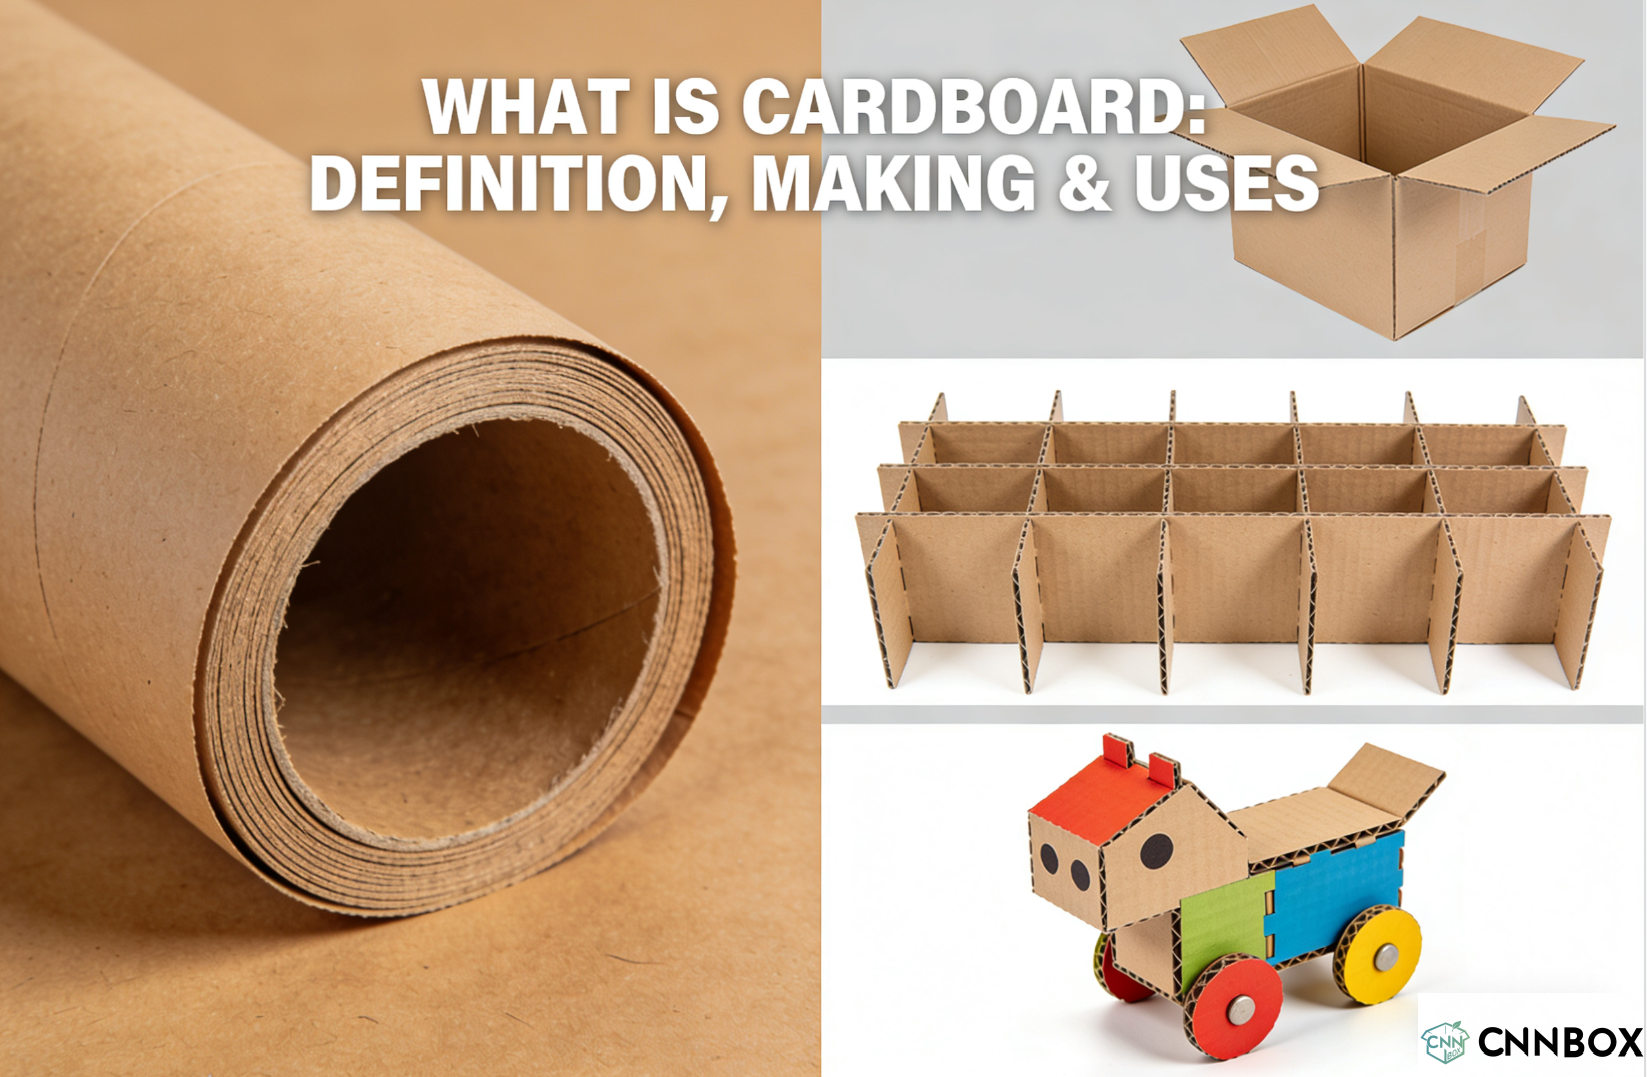
What Is Cardboard? Definition and Standards
Cardboard acts as a heavy-duty paper material. The industry defines it strictly: any board exceeding 250 g/m² in grammage and 0.3 mm in thickness. ISO standards use these weight and caliper limits to separate cardboard from regular paper stock. You might hear people use the term for everything from cereal boxes to shipping cartons. But pros draw a line. We distinguish between single-layer paperboard (like cardstock) and multi-layered corrugated board built for strength.
Classification by Structure
Solid Board is created by pressing multiple layers of pulp together. The layers are tightly bonded to form a homogeneous structure. With a smooth surface, it is ideal for high-quality printing. You’ll often see this used in high-end packaging boxes and book covers. Thickness usually ranges from 1 to 3 mm, offering excellent stiffness and compression resistance.
Corrugated cardboard is the most common type on the market. It consists of a wave-shaped core (fluting medium) sandwiched between flat surfaces (liner board). Depending on the fluting layers, it is classified as:- Single Wall: One layer of fluting + two liners, approx. 3-4 mm thick.- Double Wall: Two layers of fluting + three liners, approx. 7 mm thick.- Triple Wall: Three layers of fluting + four liners, capable of exceeding 10 mm in thickness.
Honeycomb Board utilizes a biomimetic design. The core features a hexagonal honeycomb structure. This design is incredibly lightweight yet retains high strength. Its compressive strength is 30-50% higher than corrugated board of the same weight. It is primarily used for heavy cargo pallets and architectural partitions.
Classification by Raw Material
Virgin Fiber Board is manufactured using fresh wood pulp. The fibers remain intact, providing the highest tensile strength. Kraft paper is a typical representative, with its unique brown color coming from unbleached chemical wood pulp. Edge Crush Test (ECT) values can reach 1.4 kN/m. This material is the top choice for food and pharmaceutical packaging.
Recycled Cardboard uses recovered waste paper as its primary raw material. Currently, about 80% of corrugated cardboard on the market contains recycled content. While fiber strength is slightly lower than virgin pulp, it retains essential packaging performance even after being recycled multiple times (up to 7 times). Production energy consumption is reduced by 65%, meeting sustainable development requirements.
Mixed Pulp Board balances cost and performance by mixing virgin and recycled pulp in specific ratios. For example, the outer layer might use 40% virgin pulp to ensure print quality, while the inner layer uses 60% recycled pulp to control costs. This formula is widely used in E-Commerce packaging.
Classification by Function
Waterproof Cardboard surfaces are treated with paraffin, polyethylene, or water-based coatings. The Cobb value (water absorption index) is kept below 30g/m². It can withstand short-term contact with moisture without deforming, making it suitable for cold chain logistics and beverage packaging.
Food Grade Cardboard must comply with FDA or EU standards. It contains no fluorescent whitening agents or heavy metals and passes migration tests. Pizza boxes and bakery packaging—scenarios with direct food contact—commonly use this type of board.
Fire Retardant Cardboard incorporates flame retardants like phosphates or borates. It achieves a B1 combustion rating (difficult to ignite). It is mainly used for display props and temporary partitions in public buildings.
Anti-static Cardboard has conductive fibers mixed in during production or is sprayed with anti-static agents. Surface resistance is controlled within the 10⁶-10⁹ Ohm range. Designed for electronic component packaging, it effectively prevents static electricity from damaging precision circuits.
Clarifying Confusing Concepts
Many people mistake a “box” for “cardboard.” In reality, a box is a three-dimensional container processed and formed from cardboard. “Chipboard” refers specifically to low-quality recycled board; it has a rough surface and lower strength, often used for shoe box linings.
Cardstock refers to thick paper ranging from 200-250 g/m². Its thickness sits right at the critical point between ordinary paper and cardboard. It is commonly used for business cards and greeting cards.
Understanding these differences can help you make accurate choices during procurement or usage.
Cardboard Manufacturing Processes
Creating a flat, sturdy sheet of cardboard involves three core processes: raw material preparation, forming, and post-processing. The technical parameters at each stage directly determine the final product’s performance.
Raw Material Preparation

Virgin Wood Pulp Board production begins with wood chipping. Chippers cut logs into thin flakes of 15-25 mm. These chips enter a digester where the temperature is set to 160-170°C. Chemicals (sulfate or sulfite) react with the chips for 4-6 hours to break down lignin, releasing pure cellulose fibers. The resulting pulp is dark brown. Screening removes uncooked chips. White cardboard requires a bleaching process. The overall pulp yield is about 45-50%—meaning 100 kg of wood produces about 45-50 kg of dry pulp.
Recycled Cardboard involves more steps in raw material handling. Waste paper is mixed with water in a pulper for 15-20 minutes at 40-50°C. Once fibers are fully dispersed, they enter a cleaning system. Heavy impurities are separated by gravity, while light impurities (plastics, foam) are removed via flotation. De-inking is the most critical step; surfactants and sodium hydroxide are added to detach ink particles from fibers. Air is injected into flotation tanks, causing ink to attach to bubbles and rise to the surface. This process removes 85-95% of printing ink. After 3-5 stages of screening and washing, the waste paper is converted into usable pulp.
Plant Fiber Board uses non-wood materials like wheat straw, rice straw, or bamboo. Plants are pre-treated in a biological enzyme pool for 24 hours to soften the outer wax layer. They then enter an alkaline digester at 140-150°C for 2-3 hours. Since plant fibers are short and brittle, the cooking conditions are milder than for wood pulp. The yield is typically between 35-40%.
Forming

Solid Board is produced using a multi-wire paper machine. Pulp is diluted to a 0.5-1.5% concentration and sprayed onto a high-speed forming wire (running at 200-600 meters/minute). Vacuum suction boxes beneath the wire remove over 90% of the water. The wet web’s moisture content drops to 18-22%. For multi-layer structures, additional layers of pulp are superimposed in subsequent wire sections and bonded while wet. Vacuum rolls and press rolls perform mechanical dewatering, reducing moisture to 12-15%. The board then enters the dryer section, where steam-heated cast iron cylinders (120-150°C) dry the cardboard to a final moisture content of 7-9%. The entire process from wet pulp to dry board takes only 2-3 minutes.
Corrugated Cardboard production is more precise. The medium paper (core) first passes through pre-heater rolls to reach 170-180°C, softening the fibers. It then enters the corrugating rolls—toothed metal rollers that press the flat paper into a wave shape. Flute height varies from 1.5 mm (E-flute) to 4.8 mm (A-flute). The tips of the newly formed waves are immediately coated with adhesive (corn starch or synthetic glue) at 8-12 g/m². The liner board contacts the glued flute tips and is bonded under heat and pressure (150-170°C, 0.4-0.6 MPa). The glue cures within 3-5 seconds, forming single-face corrugated board. This process is repeated for double or triple-wall boards. Modern production lines can run at 250 m/min, outputting over 1,000 square meters of cardboard per minute.
Post-Processing
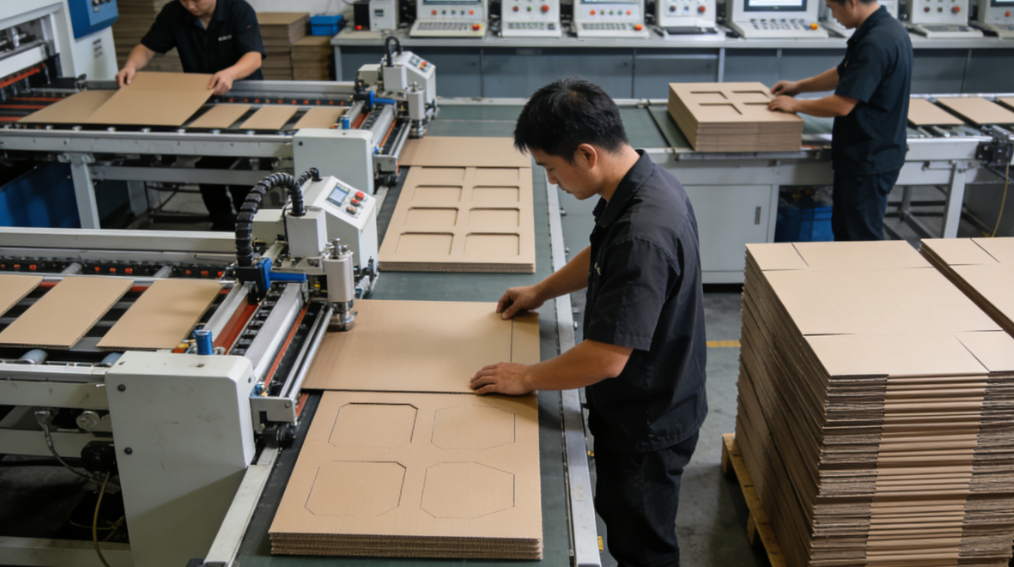
Waterproof Coating uses two mainstream technologies. Wax-based coating works via a hot melt coater, applying a 15-25 micron paraffin film to the surface. This reduces the Cobb absorption value from 120-150 g/m² to under 25 g/m². Polyethylene (PE) coating uses an extruder to laminate a molten PE film (20-40 microns) onto the board, creating a complete moisture barrier. Cardboard treated this way can withstand 95% humidity for 72 hours without deformation.
Fire Retardant Coating typically uses phosphates or intumescent agents. Spraying machines apply the retardant liquid evenly. Once dry, it forms a transparent layer. Upon contact with fire, the coating expands to create a heat-insulating carbon layer, delaying combustion. Treated cardboard sees its Oxygen Index (LOI) rise from 18-20% to 28-32%, achieving a B1 rating, though this adds 10-15% to the cost.
Creasing and Die-cutting determine the box’s structural quality. Creasing blades press indentations into the board (1/3 to 1/2 of the thickness) so fibers don’t break during folding, ensuring clean lines. Die-cutting blades cut out the board’s profile and holes. High-speed die-cutters can process 8,000-15,000 sheets per hour with a tolerance within ±0.5 mm.
Environment and Energy
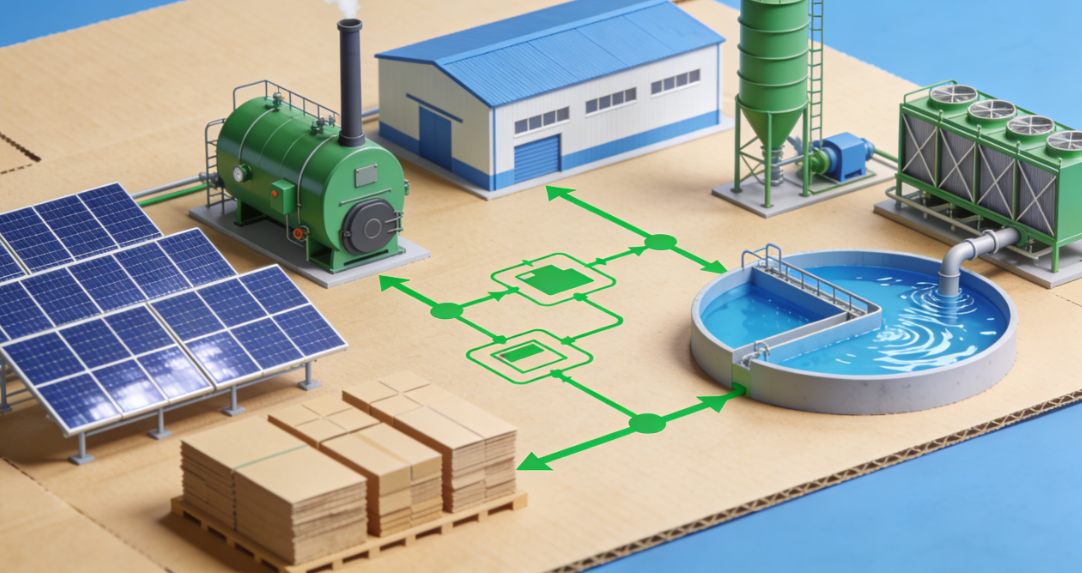
Modern board mills use a three-stage water purification system. Primary sedimentation removes suspended fibers (95% recovery). Secondary biological tanks use activated sludge to decompose organics, dropping COD (Chemical Oxygen Demand) from 800-1200 mg/L to under 100 mg/L. Tertiary treatment removes color and residual chemicals. The effluent meets industrial water standards and can be recycled, achieving an 85-90% water recycling rate. Fresh water consumption per ton of board has dropped from 50-80 tons to 8-12 tons.
Energy Optimization focuses on drying. Traditional steam cylinders have a thermal efficiency of only 60-65%. New infrared drying technology directs heat radiation straight at the board, boosting efficiency to 75-80% and cutting energy use by 20%. Condensate recovery systems capture steam from dryers to preheat incoming water, saving 0.3-0.5 tons of steam per ton of board.
Usage of recycled raw materials continues to climb. In 2023, the global corrugated industry’s waste paper utilization rate reached 82%, exceeding 90% in some European countries. One ton of waste paper produces 0.85 tons of recycled pulp, saving 3.3 tons of timber and 500-600 kWh of electricity. Fibers can be recycled 5-7 times before becoming too short for strength, after which they are used for compost or fuel.
Modern mills are also implementing Carbon Neutral Plans. Installing solar PV panels supplies 10-15% of electricity needs. Biomass boilers burn pulping waste (black liquor, bark) instead of fossil fuels, cutting carbon emissions by 40-50%. Some leading companies have achieved carbon emissions below 350 kg CO₂ equivalent per ton of board.
Uses of Cardboard
Global cardboard production exceeds 240 million tons annually. While 85% goes into packaging, the remaining 15% is spread across construction, cultural creativity, and industrial sectors. The versatility of cardboard exceeds most people’s imagination.
The Packaging Sector
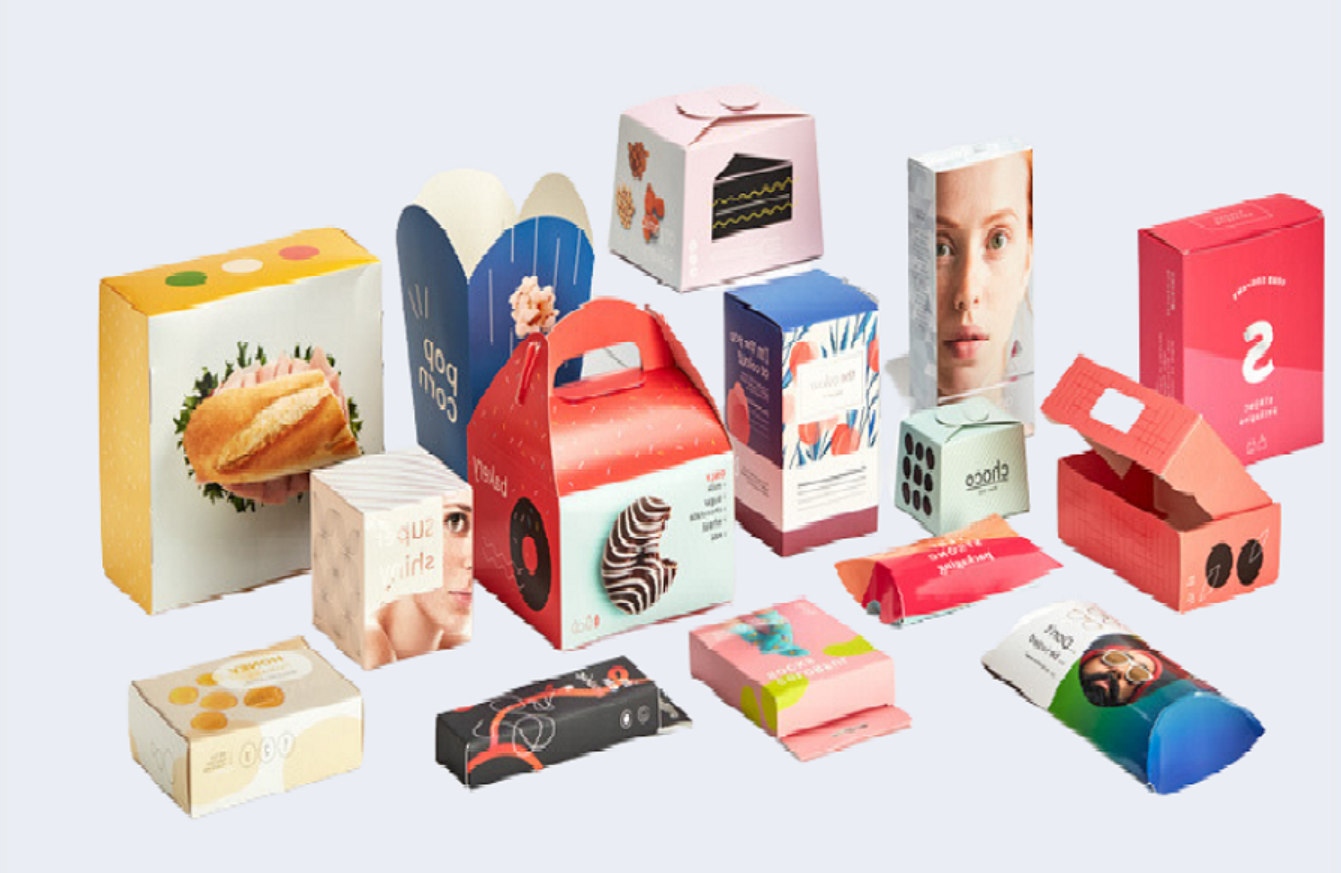
E-commerce Express Boxes consume over 40% of global corrugated output.
Platforms like Amazon and JD.com ship tens of millions of boxes daily. Standard courier boxes use BC-flute or BE-flute double-wall structures. Edge crush strength must reach 5.5-7 kN/m, capable of carrying 10-30 kg.
Internal fillers use crinkled paper or honeycomb board to buffer drop impacts. A standard No. 3 box cost is low, but after 3-5 cycles of reuse, strength drops by 30%, prompting recycling.
Food Packaging Boxes have strict hygiene requirements.
Pizza boxes use 250-350 g/m² food-grade white board coated with aqueous polyethylene. It resists grease penetration for over 24 hours and withstands microwave heating up to 120°C without deformation.
Tetra Pak for milk and beverages consists of 6 layers. The cardboard layer makes up 70%, providing structural strength. PE films inside and out provide waterproofing, while an aluminum foil layer blocks light and oxygen. This design gives shelf-stable milk a life of 6-12 months.
Gift & Luxury Packaging pursues visual texture.
Solid grey board (1.5-3 mm thick) is laminated with art paper or specialty paper. Techniques like hot stamping, UV varish, and embossing add tactile depth.
Apple product packaging uses a patented “glue-free” structure. The board forms a self-locking shape through precision die-cutting and folding. The Unboxing experience is designed as a ritual. An iPhone box costs about $3-5, representing 0.3-0.5% of the retail price.
Protective Packaging Inserts safeguard fragile goods.
Honeycomb board pads can withstand drop tests from 2-5 meters. Compressive strength reaches 8-12 MPa, yet weight is only 60% of equivalent EPS foam.
Appliance giants like Haier and Midea are replacing plastic foam en masse, eliminating tens of thousands of tons of plastic waste annually. Honeycomb pads cost 15-25% more than foam, but the brand premium and eco-friendly image yields far outweigh the cost.
Industrial and Construction

Honeycomb Cardboard Partitions are rapidly spreading in exhibitions and office renovations.
A 50-100 mm thick honeycomb panel has a sound insulation index of 30-35 dB, equivalent to 12 mm thick gypsum board, but at 1/5th the weight. Installation speed is 3 times faster.
A co-working space in Shanghai used honeycomb partitions for 500 stations. Material cost was 120-180 RMB/m², compared to 200-280 RMB/m² for traditional light steel keel gypsum board. Upon removal, the board is 100% recyclable.
Furniture Liners & Door Cores reduce costs while maintaining strength.
Brands like IKEA use honeycomb paper cores extensively. Two layers of 3 mm MDF sandwich a honeycomb core. An 18 mm thick tabletop can bear 80 kg/m² with less than 2 mm bending deformation, weighing 70% less than solid wood. Shipping costs drop significantly.
Finished door cores use a similar structure, achieving sound insulation of 28-32 dB, meeting residential standards.
Industrial Pallets & Logistics Tools show cardboard’s potential for heavy loads.
Triple-wall cardboard pallets have a static load capacity of 1000-1500 kg and a dynamic load of 500-800 kg, complying with EPAL and GMA standards.
Costs are 40-60% of wood pallets and 30-40% of plastic ones. Exports require no fumigation, saving time and fees. Coca-Cola and Unilever use paper pallets extensively in regional distribution centers.
Model Making & Soundproofing serving creative design.
Architectural models use 1-2 mm grey board, cut with 0.1 mm precision. Matte paint sprays simulate real textures.
Recording studios paste corrugated board on walls as sound absorbers. The wave structure diffuses sound waves, with a mid-high frequency absorption coefficient of 0.4-0.6. Costs are 1/3 of professional acoustic foam.
Daily Life and Cultural Creativity
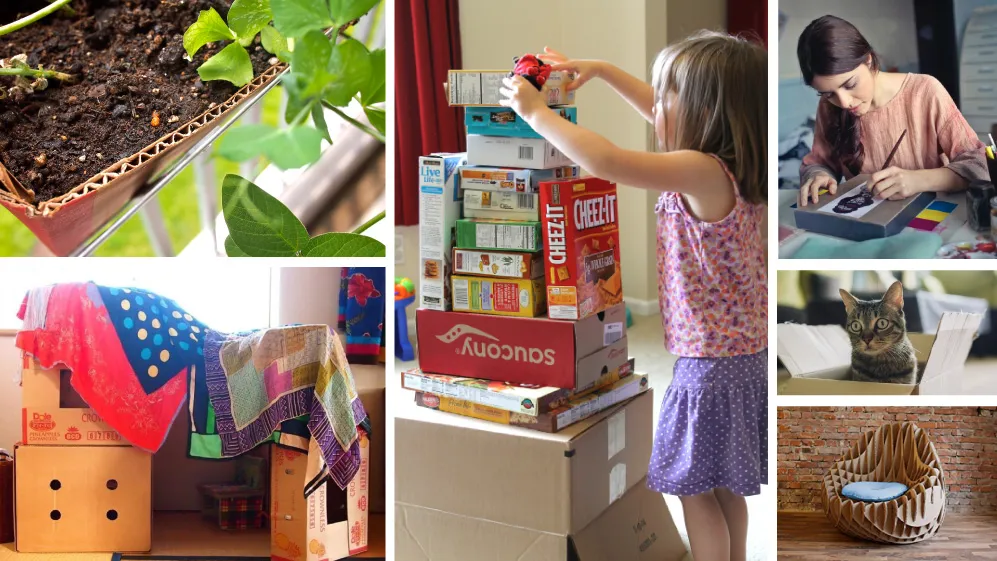
Stationery & Office Supplies bring cardboard into daily routines.
Hardcover notebooks use 250-350 g/m² grey board, laminated for durability. Folders use double grey board or white card (1-1.5 mm) for stiffness.
Archive boxes must hold 15-25 kg, with ECT >6 kN/m. Japanese brand KOKUYO’s “Campus” binders use 90% recycled board, earning the Blue Angel eco-label.
Children’s Toys & Educational Tools prioritize safety.
Toy cardboard must pass EN71 or ASTM F963 standards. Heavy metals must be below limits. Corners are die-cut round to avoid cuts.
Puzzles and blocks use food-grade white board, non-toxic even if chewed. Flashcards for education use laminated board, withstanding over 5,000 tears.
Handicrafts & DIY Culture drive a huge market.
E-commerce sales of cardboard craft kits number in the millions annually, covering themes from dinosaur models to dream castles.
Adult coloring books with hard covers and thick card pages are popular for stress relief. Social media tutorials on cardboard crafts garner millions of views, inspiring creators globally.
Cultural Products & Brand Packaging reflect cultural value.
Museums like the Forbidden City and the British Museum use custom cardboard for merchandise, printing artifact patterns and using embossing for 3D effects. Boxes cost 3-8 RMB but sell for 20-50 RMB, becoming collectibles themselves.
Indie designers use specialty cardboard (cotton or wood pulp texture) for postcards with letterpress printing, selling for a high premium.
Custom Performance Needs

Waterproof Cardboard for wet environments.
Fresh food distribution uses PE-lined corrugated boxes. With a Cobb value under 20 g/m², edge strength retains 85% after 24 hours of water immersion. Combined with ice packs, it keeps temps at 2-8°C for 48 hours. Costs are 30% lower than foam boxes, with higher recycling value.
Temporary outdoor signs use double-laminated board, lasting 3-6 months against rain and sun.
Fire Retardant Cardboard for safety compliance.
Mall displays and exhibition booths use flame-retardant board (LOI ≥32%, Smoke Density ≤75, B1 rating). Self-extinguishing time is under 5 seconds.
Costs are 20-30% higher, but it avoids safety risks and legal issues. Some regions mandate this for public spaces.
Anti-static Cardboard protecting electronics.
Chip and PCB transport requires static control. ESD cardboard has a surface resistance of 10⁶-10⁹ Ohms. Triboelectric voltage is kept under 100V.
Costs are 2-3 times that of regular board. It is standard in semiconductor and mobile manufacturing. Global consumption exceeds 500,000 tons annually.
Cardboard’s diverse applications continue to expand, from traditional packaging to high-tech fields. The balance between performance optimization and cost control drives innovation. Understanding the logic of cardboard selection helps businesses and individuals make smarter material decisions.
Summary: The Future Wrapped in Paper
We explored fibers, flutes, and cardboard uses. But this material is more than a plain brown container. It balances structural strength, cost savings, and sustainability. The world is dropping single-use plastics. Cardboard takes its place. It has grown from simple shipping boxes to high-tech, waterproof options.
Pick the right cardboard specs. A specific flute or material blend makes a difference. It stops damaged returns and creates happy customers. You aren’t just buying a box. You improve your whole supply chain.
Ready to Improve Your Packaging?
Don’t stress about the technical terms. You might need a strong box for industrial parts. Or you need a food-safe box for bakery treats. The right choice is key. Contact CNNBox team today. We help you pick the specs. You get a custom design that protects your products and helps your brand.


